Tube notching template generator: a printable coping template for any tube, angle and offset
Updated on 23 October 2026
A tube that meets another tube has to be notched, coped or fishmouthed to sit tight before it is welded: every roll cage, chassis, trailer frame, handrail and go-kart is full of these joints. The cut is a curve that depends on both tube sizes, the angle between them and how far one is offset from the other, and the reliable way to get it right is a paper template wrapped round the tube. This page draws that template for any combination and prints it at full size.
Everything runs in your browser: nothing to install, no account, and the template prints on ordinary A4 or Letter paper, tiled when it is wider than one sheet.
Tube notching template generator
Type the outside diameter of the tube you are cutting, the outside diameter of the tube it meets, the angle between them and the offset between their centre lines (0 when they are centred). The depth of the notch and the table of heights come out at once, and Print gives the template at 1:1.
| Wrap (circumference) | – |
|---|---|
| Depth of the notch | – |
| Station spacing | – |
| Station | Angle | Along the wrap | Height above the straight edge |
|---|
Drawn on the outside of both tubes, where the paper sits. 0° is the line of the tube in the plane of both tubes, on the side of the acute angle. A fraction is read as inches. Nothing is sent anywhere: the template is drawn and printed by your browser.
How to use the template
- Print at actual size, 100 %, with no fit-to-page. Measure the check bar on the sheet: it must read 100 mm or 4 in. If it does not, the printer scaled the page.
- Cut out the template along the curve. When it took more than one sheet, glue the sheets on the repeated strip at the edge, matching the curve.
- Wrap it round the end of the tube with the straight edge square to the tube, and tape it. The wrap is exactly the circumference of the tube, so the two ends meet.
- Put the 0° station on the line of the tube that lies in the plane of both tubes, on the side of the acute angle; 180° is the heel, where the cut is deepest on an angled joint. For a 90° joint without offset, any of the four quarter marks works.
- Mark along the curve with a scriber or a fine marker, take the template off and cut: grinder, band saw, hole-saw notcher or plasma. Leave the line, then dress the notch to fit on the other tube.
The formula
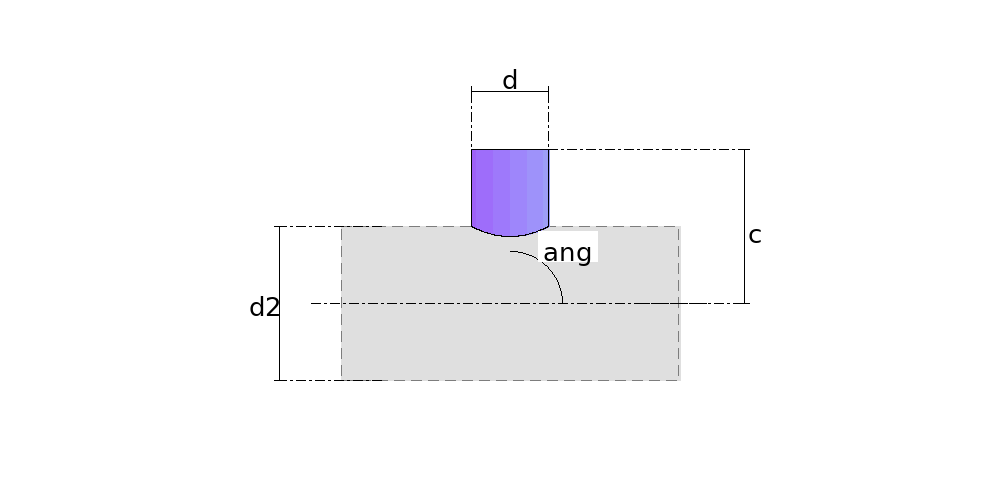
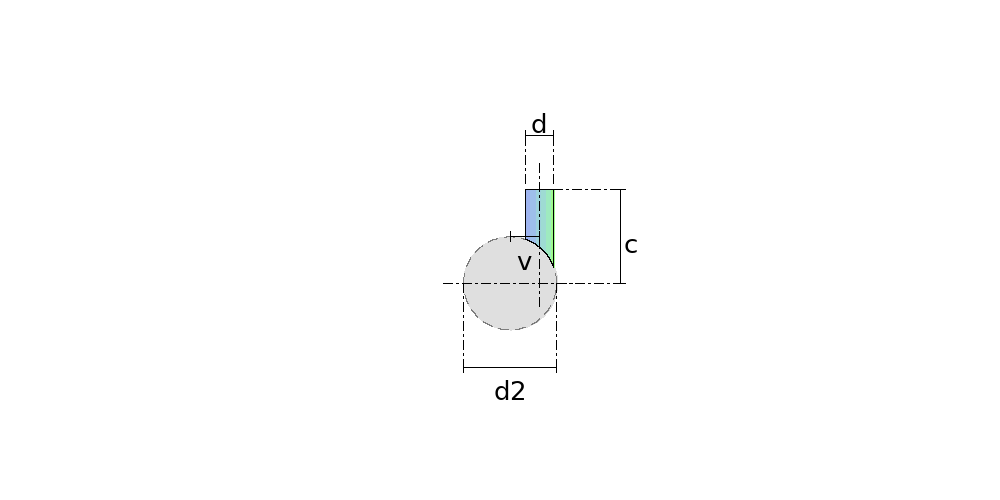
Take r as the outside radius of the tube you cut, R as the outside radius of the tube it meets, α as the angle between the two centre lines and e as the offset between them. The generator of the cut tube at angle φ round its circumference reaches the other tube at
- Notch line
ℓ(φ) = [ r × cos φ × cos α − √(R² − (r × sin φ + e)²) ] / sin αThe template height at each station is ℓ(φ) minus the lowest ℓ, plus the margin to the straight edge. The wrap is π × d, the outside circumference of the cut tube.
It is the same geometry as the pipe branch and the offset pipe branch, worked on the outside of both tubes because that is where the paper sits. Two equal tubes at 90° give the deepest centred notch: half the diameter, 0.875 in on 1-3/4 in tube. At 45° the same pair notches 2.112 in deep at the heel.
The offset has to keep the cut tube within the other one: r + e cannot exceed R. Beyond that the tubes no longer meet all round, and the joint is a different cut.
Tube sizes and wraps
The wrap of the template is the outside circumference of the tube you are cutting. For the round tube sizes used in cages, chassis and frames:
| Tube OD | Wrap | Wrap (mm) | Depth, same tube at 90° |
|---|---|---|---|
| 3/4 in | 2.356 in | 59.8 | 0.375 in |
| 1 in | 3.142 in | 79.8 | 0.500 in |
| 1-1/4 in | 3.927 in | 99.7 | 0.625 in |
| 1-1/2 in | 4.712 in | 119.7 | 0.750 in |
| 1-5/8 in | 5.105 in | 129.7 | 0.813 in |
| 1-3/4 in | 5.498 in | 139.6 | 0.875 in |
| 2 in | 6.283 in | 159.6 | 1.000 in |
| 2-1/2 in | 7.854 in | 199.5 | 1.250 in |
| 3 in | 9.425 in | 239.4 | 1.500 in |
For standard pipe sizes, from 1/2 in to 12 in, there are ready-made templates for the 90° tee, the 45° lateral and the mitre cut, as printable PDFs: start with the 2 inch pipe saddle template.
Wall thickness and plate
The template is drawn on the outside of both tubes, which is right for tube and thin-wall pipe: the notch is cut to the outside and the joint closes on the outside of the other tube. On heavy-wall pipe the inside edge of the cut also touches the other tube near the flanks; cut to the line and dress the inside with a grinder until it seats.
A branch rolled from flat plate is a different job: its pattern is worked on the mid-thickness of the plate, and the pipe branch calculator does that one, with the flat pattern, the 1:1 template and the DXF.
Frequently asked questions
- How do I make a tube notching template?
- Type the two tube outside diameters, the angle and the offset in the generator above and print the template at 100 %. Wrap it round the tube end with the straight edge square, mark the curve and cut to the line.
- What is the difference between notching, coping and fishmouthing?
- None: they are three names for the same saddle-shaped cut on the end of a tube that lets it sit on another tube.
- Which way round does the template go?
- 0° on the line of the tube in the plane of both tubes, on the acute side; 180° is the heel, where an angled notch is deepest. On a 90° joint without offset the template is symmetric and any quarter mark lines up.
- Does the wall thickness change the template?
- Not for a template wrapped round the tube: it is drawn on the outside, where the paper sits. On heavy-wall pipe, dress the inside edge of the notch after cutting.
- Why does the printed template not fit round my tube?
- The printer scaled it. Print at actual size, 100 %, and check the bar on the sheet: 100 mm or 4 in. Also check the tube with a calliper: a 1-3/4 in tube is 1.750 in outside, and the wrap is 5.498 in.
Parts in this guide
Other guides
- How to develop a cone (frustum) in sheet metal: formula, sector radii and angle, step by step
- Lobster back bend calculator (segmented 90° elbow): gore angles, cut heights and how many plates
- Pipe saddle calculator and development: how to lay out a pipe-to-pipe branch (tee) at 90 and 45 degrees
- Square to round transition: development by triangulation, step by step
- The neutral axis of plate: why every development uses D − t, and the bend deduction
- Sheet metal glossary: the terms of marking out and pattern development in plate fabrication
- How we check the Planichapa calculations, and who is behind them
- LITIO alternative: Planichapa develops sheet metal parts in the browser, nothing to install, now that LITIO2 is no longer sold
- How to lay out a mitre-cut pipe: paper template, sine wave and ordinate table
- Plate 'n' Sheet alternative: Planichapa develops sheet metal parts in the browser, with the price on the page
- Steel plate weight calculator, weight per m², gauges and stock plate sizes: table and formula
- Pipe ovality: a calculator, the formula, a worked example, the limits the codes use and how to measure it in the shop
- Sheet metal pattern development software: how to choose, and what changes between a desktop program, a phone app and an online calculator
- Eccentric and concentric reducers: which one to use and how each one develops on plate
- Roller chain size chart: ANSI, ISO 606, motorcycle and bicycle chain pitch and roller diameter
- Sprocket dimensions: pitch diameter, outside and root diameter, tooth form and a pitch diameter chart
- Bolt circle layout: the position of each hole, the chord between holes and a chord chart
- Chain length and sprocket ratio: the formulas, a worked example and how many links to cut
- Screw flight calculator: the flat blank of a screw conveyor flight (auger), with the formula and a worked example
- Plate rolling calculator: the blank length of a rolled shell, with the formula, a chart and a worked example
- Dished head calculator: depth, volume, blank diameter and weight of torispherical, 2:1 elliptical and hemispherical heads
- Cone template generator: a printable full-size cone template for hoppers, funnels and reducers
- Pie cut calculator for exhaust and tube bends: saw angle, pie lengths and a wrap-around template
- Duct transition layout: square to round duct, centred, offset or flat on one side
- Pipe template, printable at full size: tee saddle, 45° lateral and mitre cut for every pipe size from NPS 1/2 to 12
- Register boot layout: from a floor, wall or ceiling register to a round duct, in inches
- Plenum box and plenum transition layout: the sides, the offset and the round outlet