Plate rolling calculator: the blank length of a rolled shell, with the formula, a chart and a worked example
Updated on 23 October 2026
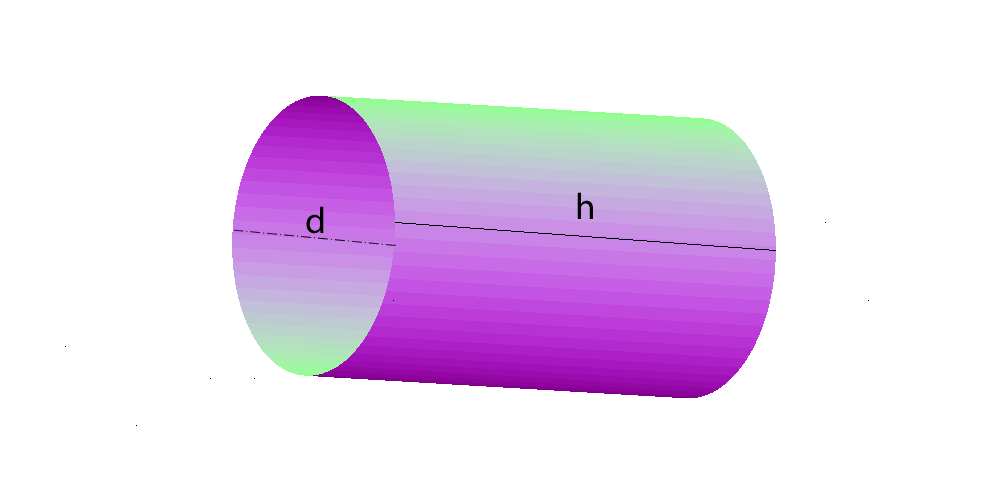
Rolling a shell starts with one number: how long to cut the plate. Cut it to the outside circumference and the shell will not close; cut it to the inside and it gaps. The right length is the circumference at mid-thickness, and this page gives it for any diameter and plate, with the shell weight, the number of stock plates it takes, a chart and the formula.
The cylinder calculator draws the blank, with the 1:1 template and the DXF for the cutting table.
Plate rolling calculator
Pick which diameter your drawing gives, type it and the plate thickness. The shell height and the stock plate length are optional: with them come the weight and how many plates go round.
| Mean diameter (neutral axis) | – |
|---|---|
| Blank length to cut | – |
| Too long if worked on the outside diameter | – |
| Shell weight | – |
| Stock plates round the shell | – |
The blank is the circumference on the neutral axis, at mid-thickness: π × (outside diameter − t). A fraction is read as inches in any field. Nothing is sent anywhere: the sums run in your browser.
Open this shell in the cylinder calculator: drawing, 1:1 template and DXF
The formula
When plate is rolled, the outside of the wall stretches and the inside is squeezed. In the middle there is a fibre that does neither, the neutral axis, and its length is the length of the flat blank. For rolling, where the diameter is many times the thickness, the neutral axis sits at mid-thickness.
- Blank length
L = π × (D − t) = π × (d + t) = π × DmD is the outside diameter, d the inside diameter, Dm the mean diameter and t the plate thickness. All three forms give the same length.
- What the outside diameter gets wrong
π × D − L = π × tWorked on the outside diameter, the blank comes out π × t too long, whatever the diameter: 19.95 mm on 1/4 in plate, 0.785 in.
- Shell weight
kg = L (m) × h (m) × t (mm) × 7.85h is the shell height, the width of the plate; 7.85 kg/dm³ is carbon steel. In pounds: L (in) × h (in) / 144 × the weight per square foot of the plate.
The neutral axis and thickness guide explains why the middle of the wall, and when it moves.
Worked example
A shell of 1000 mm outside diameter, 1500 mm high, in 6.35 mm (1/4 in) carbon steel plate, from 3000 mm stock plates:
- Mean diameter: 1000 − 6.35 = 993.65 mm.
- Blank length: π × 993.65 = 3121.64 mm. Worked on the outside diameter it would be 3141.59 mm, 19.95 mm too long.
- Weight: 3.12164 × 1.5 × 6.35 × 7.85 = 233.4 kg.
- Stock plates: 3121.64 mm does not fit in one 3000 mm plate, so the shell takes 2 plates and 2 longitudinal seams; from a 6000 mm plate, 1 plate and 1 seam.
The same in inches: a 48 in outside diameter tank shell, 60 in high, in 1/4 in plate. Mean diameter 47.75 in, blank length π × 47.75 = 150.01 in (12 ft 6 in), 0.785 in shorter than the outside circumference, and 638 lb of plate.
Blank length chart
Blank length for common shells, from the outside diameter, on the neutral axis. Metric, in millimetres:
| Outside diameter | t 3 mm | t 6.35 mm | t 9.53 mm | t 12.7 mm |
|---|---|---|---|---|
| 300 mm | 933.1 | 922.5 | 912.5 | 902.6 |
| 500 mm | 1561.4 | 1550.8 | 1540.9 | 1530.9 |
| 1000 mm | 3132.2 | 3121.6 | 3111.7 | 3101.7 |
| 1500 mm | 4703.0 | 4692.4 | 4682.4 | 4672.5 |
| 2000 mm | 6273.8 | 6263.2 | 6253.2 | 6243.3 |
| 3000 mm | 9415.4 | 9404.8 | 9394.8 | 9384.9 |
In inches:
| Outside diameter | 1/8 in | 3/16 in | 1/4 in | 3/8 in | 1/2 in |
|---|---|---|---|---|---|
| 12 in | 37.31 | 37.11 | 36.91 | 36.52 | 36.13 |
| 24 in | 75.01 | 74.81 | 74.61 | 74.22 | 73.83 |
| 36 in | 112.70 | 112.51 | 112.31 | 111.92 | 111.53 |
| 48 in | 150.40 | 150.21 | 150.01 | 149.62 | 149.23 |
| 60 in | 188.10 | 187.91 | 187.71 | 187.32 | 186.92 |
| 72 in | 225.80 | 225.61 | 225.41 | 225.02 | 224.62 |
| 96 in | 301.20 | 301.00 | 300.81 | 300.41 | 300.02 |
What the formula does not tell
- The weld gap. If the seam needs a root gap, cut the blank that much shorter: for a 2 mm gap on the example shell, 3119.64 mm.
- The flat ends. A roll cannot bend the plate right to its edge. On a three-roll pyramid machine the ends stay flat for roughly half the distance between the bottom rolls; on initial-pinch and four-roll machines much less. Pre-bend the ends on a press brake or with a bending plate, or leave the blank long and trim the flats after rolling. Your roll's manual gives the flat for its geometry.
- Thick plate on a small diameter. When the diameter is only a few times the thickness, the neutral axis moves a little towards the inside and the plate thins on the outside. Roll a trial piece and measure before cutting the whole batch.
- Cones are not shells. A rolled cone is a sector, not a rectangle; the cone development guide gives its radii and angle.
Frequently asked questions
- How do you calculate the length of plate to roll a cylinder?
- Multiply the mean diameter by π: L = π × (outside diameter − thickness), or π × (inside diameter + thickness). A 1000 mm outside diameter shell in 6.35 mm plate needs a 3121.64 mm blank.
- Do I use the inside or the outside diameter?
- Neither: the mean one, at mid-thickness. Using the outside diameter makes the blank π × t too long and the seam overlaps; using the inside diameter makes it π × t too short and the seam gaps.
- How much plate do I need to roll a 48 inch tank?
- For a 48 in outside diameter in 1/4 in plate, the blank is 150.01 in long, 12 ft 6 in: π × 47.75. A 120 in plate is not long enough, so the shell takes two plates and two seams, or one 240 in plate.
- Why does my rolled shell overlap?
- Almost always because the blank was worked on the outside diameter: it is π × t too long, 0.39 in on 1/8 in plate. Work the length on the mean diameter.
Parts in this guide
Other guides
- How to develop a cone (frustum) in sheet metal: formula, sector radii and angle, step by step
- Lobster back bend calculator (segmented 90° elbow): gore angles, cut heights and how many plates
- Pipe saddle calculator and development: how to lay out a pipe-to-pipe branch (tee) at 90 and 45 degrees
- Square to round transition: development by triangulation, step by step
- The neutral axis of plate: why every development uses D − t, and the bend deduction
- Sheet metal glossary: the terms of marking out and pattern development in plate fabrication
- How we check the Planichapa calculations, and who is behind them
- LITIO alternative: Planichapa develops sheet metal parts in the browser, nothing to install, now that LITIO2 is no longer sold
- How to lay out a mitre-cut pipe: paper template, sine wave and ordinate table
- Plate 'n' Sheet alternative: Planichapa develops sheet metal parts in the browser, with the price on the page
- Steel plate weight calculator, weight per m², gauges and stock plate sizes: table and formula
- Pipe ovality: a calculator, the formula, a worked example, the limits the codes use and how to measure it in the shop
- Sheet metal pattern development software: how to choose, and what changes between a desktop program, a phone app and an online calculator
- Eccentric and concentric reducers: which one to use and how each one develops on plate
- Roller chain size chart: ANSI, ISO 606, motorcycle and bicycle chain pitch and roller diameter
- Sprocket dimensions: pitch diameter, outside and root diameter, tooth form and a pitch diameter chart
- Bolt circle layout: the position of each hole, the chord between holes and a chord chart
- Chain length and sprocket ratio: the formulas, a worked example and how many links to cut
- Screw flight calculator: the flat blank of a screw conveyor flight (auger), with the formula and a worked example
- Tube notching template generator: a printable coping template for any tube, angle and offset
- Dished head calculator: depth, volume, blank diameter and weight of torispherical, 2:1 elliptical and hemispherical heads
- Cone template generator: a printable full-size cone template for hoppers, funnels and reducers
- Pie cut calculator for exhaust and tube bends: saw angle, pie lengths and a wrap-around template
- Duct transition layout: square to round duct, centred, offset or flat on one side
- Pipe template, printable at full size: tee saddle, 45° lateral and mitre cut for every pipe size from NPS 1/2 to 12
- Register boot layout: from a floor, wall or ceiling register to a round duct, in inches
- Plenum box and plenum transition layout: the sides, the offset and the round outlet