Elbow flat pattern
What it is
The elbow is the two-gore bend: two half shells cut at an angle and welded to each other. It is the cheapest direction change in plate, with a single circumferential weld.
Where it is used
Offsets in exhaust and ventilation, discharges, short connections where there is no room for a larger radius.
Measurements the calculation needs
- D Outside diameter of the tube
- X Leg 1 (inside corner to mouth)
- Y Leg 2 (inside corner to mouth)
- DV Divisions
- THK Plate thickness
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Units: mm inches
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Outside diameter of the tube | 7-7/8" (7.874) |
|---|---|
| Leg 1 (inside corner to mouth) | 1-15/16" (1.9685) |
| Leg 2 (inside corner to mouth) | 7-7/8" (7.874) |
| Divisions | 16 |
| Plate thickness | 3/8" (0.3937) |
| The flat pattern fits a plate of | 23-1/2" × 15-9/16" |
| Flat patterns produced | 2 |
Result of the example
| Plate 1 | 23-1/2" × 9-5/8" |
|---|---|
| Area and weight | 0.96 ft² · ≈ 15.5 lb in 3/8" steel |
| Plate 2 | 23-1/2" × 15-9/16" |
| Area and weight | 1.9 ft² · ≈ 31.0 lb in 3/8" steel |
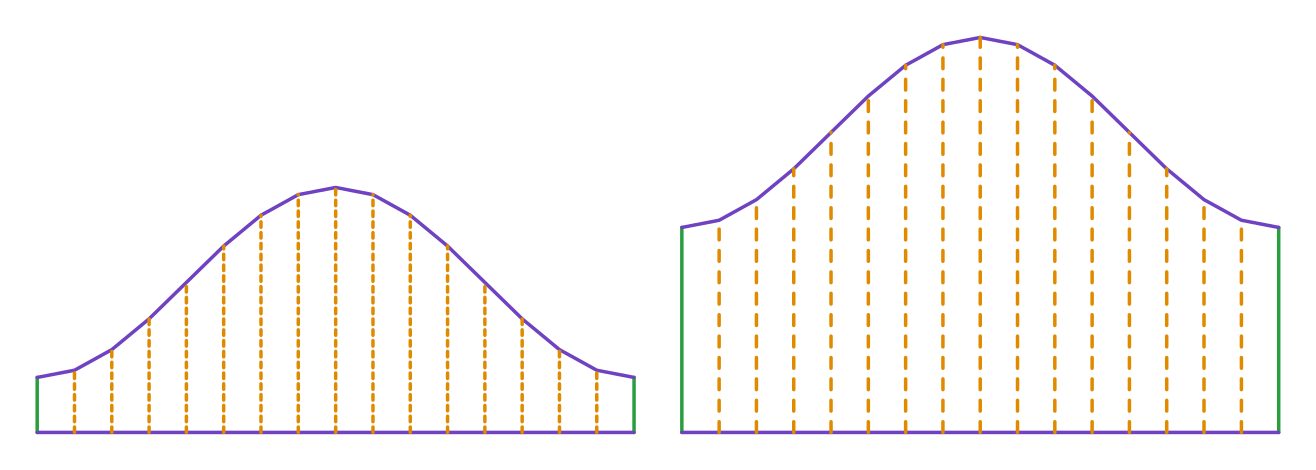
Ordinate table
| # | Position on the plate | Element height |
|---|---|---|
| 1 | 0" | 2-3/16" |
| 2 | 1-7/16" | 2-7/16" |
| 3 | 2-15/16" | 3-1/4" |
| 4 | 4-3/8" | 4-1/2" |
| 5 | 5-7/8" | 5-7/8" |
| 6 | 7-5/16" | 7-5/16" |
| 7 | 8-13/16" | 8-9/16" |
| 8 | 10-1/4" | 9-3/8" |
| 9 | 11-3/4" | 9-5/8" |
| 10 | 13-1/4" | 9-3/8" |
| 11 | 14-11/16" | 8-9/16" |
| 12 | 16-3/16" | 7-5/16" |
| 13 | 17-5/8" | 5-7/8" |
| 14 | 19-1/8" | 4-1/2" |
| 15 | 20-9/16" | 3-1/4" |
| 16 | 22-1/16" | 2-7/16" |
| 17 | 23-1/2" | 2-3/16" |
How to mark it out on the plate
- The 90° elbow is two half shells cut at 45°: each half is the truncated cylinder with α = 45°, and the two legs X and Y give the length of each half.
- Mark each half as a truncated cylinder: a rectangle of π × (D − t) by the high side, dv elements, a sine wave of amplitude (D − t) × tan 45° = D − t.
- Roll both halves, turn one half a turn against the other and weld the circumferential joint: a single seam.
Common mistakes and tolerances
- Taking the legs along the heel
- X and Y are measured from where the AXES meet to each opening. Along the heel each leg looks D/2 shorter.
- Seams on the same side
- With both longitudinal seams in line, the longitudinal weld crosses the circumferential one at the most stressed point of the elbow. Turn one half round.
Guides about this part
- Lobster back bend calculator (segmented 90° elbow): gore angles, cut heights and how many plates
- How to lay out a mitre-cut pipe: paper template, sine wave and ordinate table
- Pie cut calculator for exhaust and tube bends: saw angle, pie lengths and a wrap-around template
- Pipe template, printable at full size: tee saddle, 45° lateral and mitre cut for every pipe size from NPS 1/2 to 12
Frequently asked questions
- How does the elbow differ from a segmented bend?
- The elbow is the two-gore case. It is quicker to make, but the change of direction is abrupt and pressure loss is higher than with more segments.
- What are X and Y?
- The two legs of the elbow, measured from where the axes meet to each opening. Together they set the offset angle.
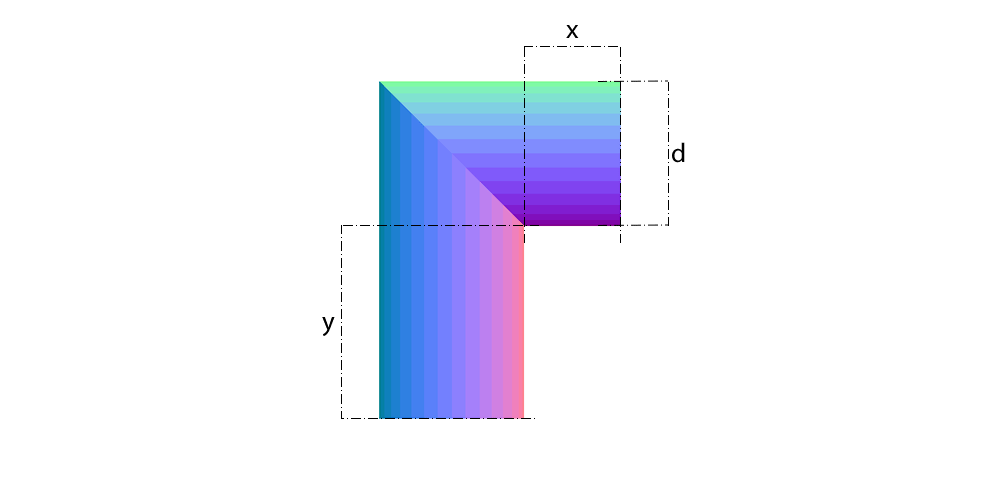
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.