Rectangular Duct Bend development
What it is
The mitred bend with its section changed: a rectangular duct instead of a round shell. The cut is the same calculation as the round bend — the mitre height at a point is its distance from the bend axis times the tangent of half the angle per gore. What changes is the path: on the round one that distance varies as a cosine and the cut comes out a sine wave; here it is constant on two faces and varies linearly on the other two.
Where it is used
Extraction and air-conditioning ductwork, dust collection runs, ventilation trunking, any change of direction in rectangular section.
Measurements the calculation needs
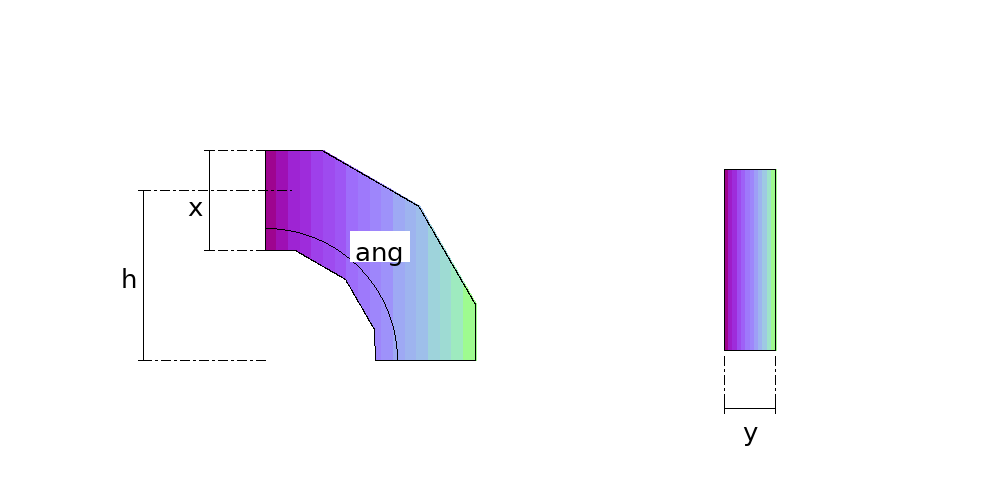
- H Radius to the bend axis
- X Side from throat to heel
- Y Side between the cheeks
- ANG Total angle of the bend
- S Number of gores
- THK Plate thickness
- R Bend radius
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Radius to the bend axis | 800 mm |
|---|---|
| Side from throat to heel | 500 mm |
| Side between the cheeks | 300 mm |
| Total angle of the bend | 90° |
| Number of gores | 3 |
| Plate thickness | 1.5 mm |
| Bend radius | 0 mm |
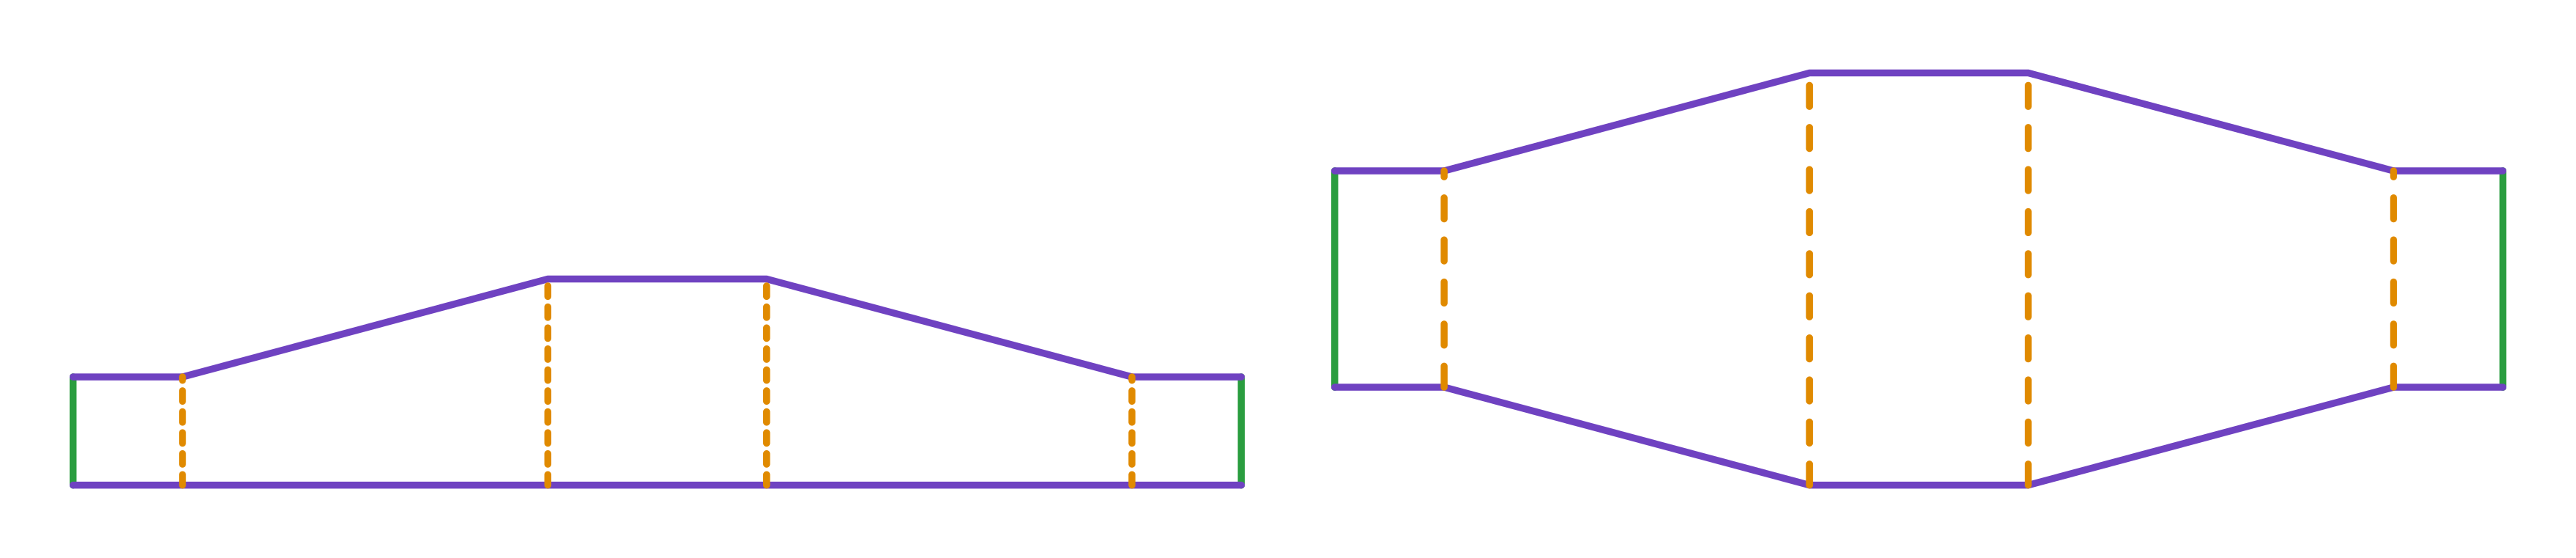
| The flat pattern fits a plate of | 1594 × 562 mm |
| Flat patterns produced | 2 |
Result of the example
| Plate 1 | 1594 × 281 mm, cut 2 times |
|---|---|
| Plate 2 | 1594 × 562 mm, cut 2 times |
Assembly notes
Weld the sheets with the longitudinal seams 180° apart, not lined up. Lined up, the piece assembles into a different shape — and the longitudinal seam crosses the circumferential one.
The pattern develops the SHARP CORNER, on the mean line — the theoretical layout, which is what gets delivered. If you fold it on a press brake with an inside radius, the blank comes out LONG: each fold needs the deduction 2*(r+t)*tan(a/2) − a*(r + k*t), with r the inside radius, a the bend angle in radians, and your tooling's k. On a 500x300 tube in 1.5 mm sheet with four 90° folds that is 3.5 mm at radius 0.75 and 9.0 mm at radius 4.5 — always to be taken off. A welded corner from separate plates needs no deduction at all.
Fold to an angle of 90° BETWEEN THE TWO FACES — what a protractor reads on the finished part, not the press stroke angle. Every crease on this part has the same angle.
Frequently asked questions
- Are all four faces of a gore cut the same?
- No, and that is the classic mistake on this part. The throat and heel faces come out RECTANGULAR, cut square, however tight the bend — each of them lies wholly at one distance from the axis, so the cut does not vary along it. Only the two side faces come out trapezoidal.
- Where is the radius measured to?
- To the bend axis, at the centre of the section. The throat is half of X inside it and the heel half of X outside, and that difference is what makes the heel come out longer than the throat.
- Why are there two sheets?
- Because the end gores are cut once and the middle ones twice. The first sheet comes in two copies — the two half-ends — and the second in one fewer than the number of gores. With a single gore the part is just the two half-ends, and the second sheet does not exist.
- Is there a limit to the angle per gore?
- Ninety degrees, the same as the round bend. At that point the half-mitre reaches 45 degrees, which is the single-cut mitred elbow. Past it the cut is steeper than 45 degrees and the part stops being makeable — anyone needing more turn adds gores.
An account is required. The free tier covers 20 calculations a month.