Cylinder flat pattern
What it is
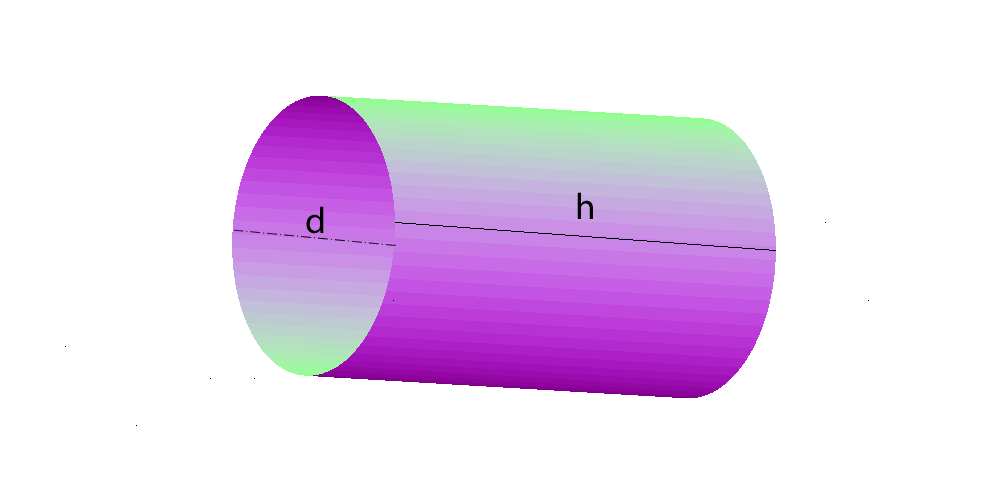
The rolled shell is the straight tube: a plate run through the rolls until both edges meet, closed with one longitudinal weld. It is the simplest part in the trade and the basis of nearly everything else — stacks, ducts, silos and tank shells are stacked cylinders.
Where it is used
Exhaust ducting, chimneys, tank and vessel shells, equipment jackets, large-diameter pipe fabricated from plate.
Measurements the calculation needs
- D Outside diameter
- H Height of the shell (its length)
- THK Plate thickness
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Units: mm inches
How it develops: the formulas
- Plate length (circumference on the neutral axis)
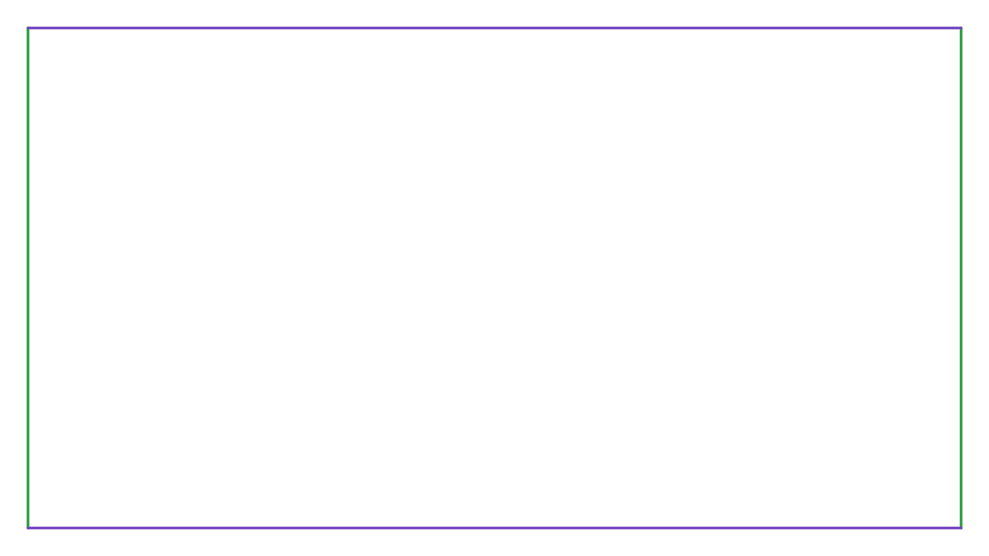
L = π × (D − t)D is the outside diameter and t the plate thickness. For D = 300 and t = 3: L = π × 297 = 933.1 mm. With π × D the plate would come out 9.4 mm long.- Plate height
H = hThe shell height goes in as it is: the plate is a rectangle of L by h.- Mean diameter
Dm = D − tThe diameter of the neutral axis, at mid-thickness. From an inside diameter use Dm = Di + t.
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Outside diameter | 11-13/16" (11.811) |
|---|---|
| Height of the shell (its length) | 19-11/16" (19.685) |
| Plate thickness | 1/8" (0.1181) |
| The flat pattern fits a plate of | 36-3/4" × 19-11/16" |
Result of the example
| Plate | 36-3/4" × 19-11/16" |
|---|---|
| Area and weight | 5.0 ft² · ≈ 24.2 lb in 1/8" steel |
How to mark it out on the plate
- Work out L = π × (D − t) and mark a rectangle of L by h on the plate. Check squareness by the diagonals: both must measure √(L² + h²).
- Mark the centre line and, if the shell takes a nozzle or branch, its position relative to the seam, before rolling.
- Cut and bevel the longitudinal seam to suit the welding process. The template is the finished part, with no root gap.
- Pre-bend both ends in the press before rolling, or leave stock and trim afterwards: a three-roll bender leaves the ends flat.
- Roll until the two edges meet, check the outside circumference with a tape (π × D) and weld the seam.
Common mistakes and tolerances
- Using the outside diameter for the circumference
- π × D instead of π × (D − t) leaves π × t over: 9.4 mm on a 300 mm shell in 3 mm plate and 31.4 mm on 800 mm in 10 mm. The seam overlaps and the shell goes oval.
- Forgetting the weld allowance
- The template is the finished part on the neutral axis. Bevel, root gap and machining stock go on top, to shop practice.
- Flat ends off the rolls
- The first and last 50 to 100 mm stay flat on a three-roll bender. Either pre-bend the ends in the press or roll with stock and trim; otherwise the seam sits on a flat and the tube comes out with a peak.
- Checking by diameter instead of circumference
- A 1 mm error in circumference is 0.32 mm in diameter. On a large shell the tape on the circumference is more sensitive than callipers on the diameter.
Guides about this part
- The neutral axis of plate: why every development uses D − t, and the bend deduction
- How we check the Planichapa calculations, and who is behind them
- LITIO alternative: Planichapa develops sheet metal parts in the browser, nothing to install, now that LITIO2 is no longer sold
- Plate 'n' Sheet alternative: Planichapa develops sheet metal parts in the browser, with the price on the page
- Steel plate weight calculator, weight per m², gauges and stock plate sizes: table and formula
- Pipe ovality: a calculator, the formula, a worked example, the limits the codes use and how to measure it in the shop
- Plate rolling calculator: the blank length of a rolled shell, with the formula, a chart and a worked example
- Dished head calculator: depth, volume, blank diameter and weight of torispherical, 2:1 elliptical and hemispherical heads
Frequently asked questions
- Why is the plate length not π times the outside diameter?
- Because the plate neither stretches nor compresses at the neutral axis, which sits at mid-thickness. The correct length is π times the mean diameter — the outside diameter less one thickness. On a 300 mm shell in 3 mm plate that is over 9 mm, more than enough to leave the weld short.
- Does the flat pattern include weld preparation?
- No. The result is the finished part on the neutral axis. If your process needs a bevel, root gap or extra stock, add it to the calculated figure according to your shop practice.
- What plate length does a 300 mm shell in 3 mm plate take?
- π × (300 − 3) = 933.1 mm, by 500 high. With the outside diameter, π × 300 = 942.5: nine millimetres over, which overlap at the seam.
- How do I check the diameter after rolling?
- By the outside circumference, with a tape, which must give π × D. A 1 mm error in circumference is only 0.32 mm in diameter, so on a large shell the tape is more sensitive than callipers.
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.