Chinese Hat flat pattern
What it is
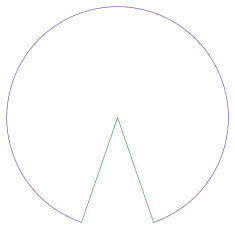
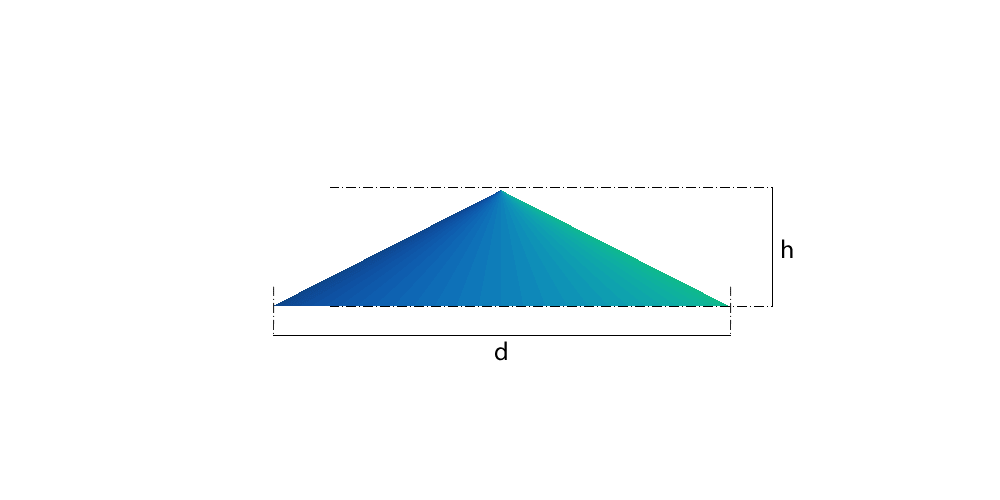
The conical cap is a full cone with no smaller opening: a disc with a wedge removed, closed into a cone. It is a cover, so it is almost always made in thin plate. The development is a disc sector whose angle depends only on the diameter and the height.
Where it is used
Chimney and vent caps, rain covers on vertical ducting, conical silo tops.
Measurements the calculation needs
- H Vertical height, apex to rim
- D Diameter of the rim
- THK Plate thickness
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Units: mm inches
How it develops: the formulas
- Outside slant height
g = √( (D/2)² + h² )For D = 200 and h = 50: g = 111.8 mm.- Mean-surface radius at the rim
rm = D/2 − (t/2) × h / gThe offset is normal to the surface, as on the cone. In the example, 3 mm plate: rm = 99.33 mm.- Sector radius (mean slant)
R = g − (t/2) × h / (D/2)In the example: 111.05 mm. It is the compass radius.- Sector angle
θ = 360° × rm / RIn the example: 322.0°. The wedge to remove is 360° − θ = 38.0°.
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Vertical height, apex to rim | 50 mm |
|---|---|
| Diameter of the rim | 200 mm |
| Plate thickness | 3 mm |
| The flat pattern fits a plate of | 222 × 216 mm |
Result of the example
| Plate | 222 × 216 mm |
|---|---|
| Area and weight | 0.035 m² · ≈ 0.82 kg in 3 mm steel |
| Arc radii | 111.1 mm |
| Sector angle | 322° |
How to mark it out on the plate
- Work out R and θ. Scribe a circle of radius R; the centre is the apex of the cap.
- Mark the angle θ from any radius or, easier in the shop, mark the arc length 2π × rm along the circle, which is the rim circumference on the mean surface.
- Scribe the two radii that close the sector: they are the two sides of the seam.
- Cut the wedge out, form by pulling one end over the other and weld the seam from apex to rim.
Common mistakes and tolerances
- Entering the slant as the height
- h is the vertical height from apex to rim. The slant is longer, and entering it makes the cap taller and tighter.
- Thinking a sector over 300° is a mistake
- It is normal: the shallower the cap, the closer the sector gets to a full disc. A 200 by 50 cap gives 322°; only 38° comes out.
- Taking t/2 off the radius in thick plate
- On an 800 by 60 cap in 20 mm plate, t/2 off the radius returns a part 783 mm across: 17 mm short. In thin plate the difference is a tenth of a millimetre.
Guides about this part
- How to develop a cone (frustum) in sheet metal: formula, sector radii and angle, step by step
- The neutral axis of plate: why every development uses D − t, and the bend deduction
- Cone template generator: a printable full-size cone template for hoppers, funnels and reducers
Frequently asked questions
- Why does the sector sometimes exceed 300 degrees?
- The shallower the cap relative to its diameter, the closer the development gets to a full disc. A very shallow cap can give a sector of 330 degrees or more, leaving only a narrow wedge to remove.
- Which height should I enter?
- The vertical height from apex to rim, not the slant length. The calculation derives the slant from it.
- What are the compass radius and sector angle in the example?
- For 200 diameter, 50 high and 3 mm plate, the sector radius is 111.05 mm and the angle 322.0°. The wedge removed is 38°.
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.