Segmented Bend development
What it is
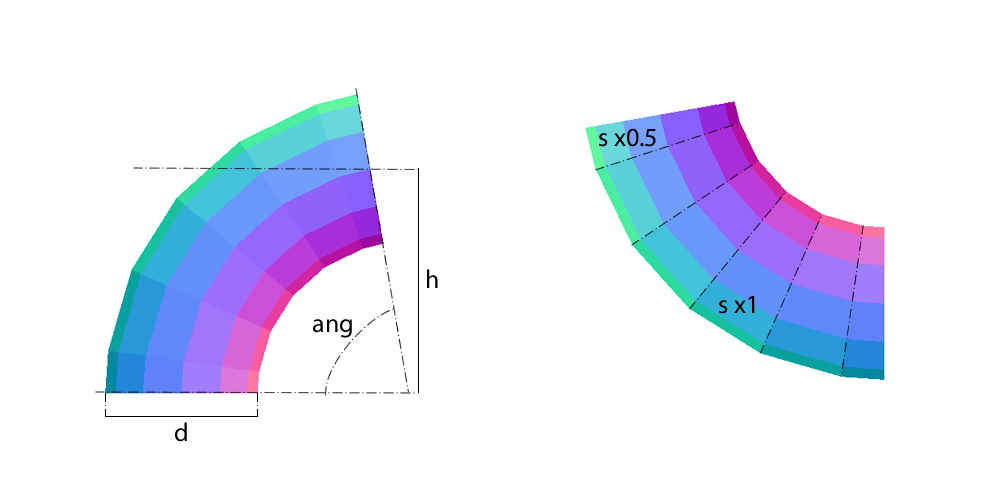
A segmented bend -- a lobster back, in British shops -- is built from lengths of tube cut at an angle and welded together, approximating a radius with straight pieces. Each intermediate gore is a cylinder cut at both ends; the two end gores take a single cut. The more gores, the smoother the bend.
Where it is used
Large-diameter bends in exhaust and ventilation, boiler ducting, process pipework where no forged elbow exists in the required size.
Measurements the calculation needs
- H Bend radius (to the tube axis)
- D Outside diameter of the tube
- ANG Total angle of the bend
- S Number of gores
- DV Divisions
- THK Plate thickness
How it develops: the formulas
- Mean radius and plate length
r = (D − t) / 2 ; L = π × (D − t)In the example, D = 800 in 10 mm plate: r = 395 mm and L = 2481.9 mm.- Half-mitre (cut angle of each gore)
β = total angle / (2 × gores)For 80° in 5 gores: β = 8°. Each middle gore turns 2β; the two end gores turn β.- Cut height at each element
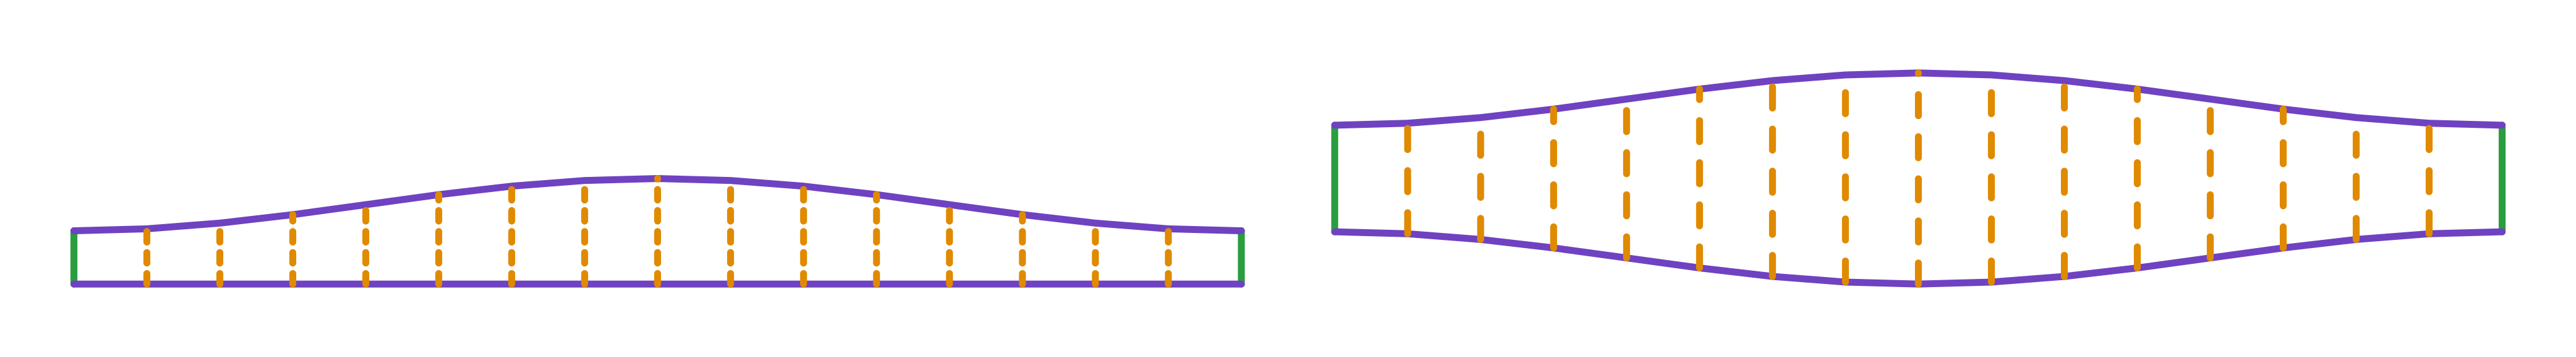
y(φ) = (R + r × cos φ) × tan βR is the bend radius at the axis and φ the angle round the tube, φ = 0 at the heel and 180° at the throat. Throat: (R − r) × tan β = 113.1 mm; heel: (R + r) × tan β = 224.2 mm in the example.- Middle gore
height = 2 × y(φ)The middle gore is cut at both ends: 448 mm at the heel and 226 mm at the throat in the example.- How many plates to cut
ends: 2 ; middles: gores − 1With 5 gores: 2 half ends and 4 full gores. With 1 gore the bend is just the two ends: the elbow. The shop's 3 gores plus 2 half gores is gores = 4 here.
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Bend radius (to the tube axis) | 1200 mm |
|---|---|
| Outside diameter of the tube | 800 mm |
| Total angle of the bend | 80° |
| Number of gores | 5 |
| Divisions | 16 |
| Plate thickness | 10 mm |
| The flat pattern fits a plate of | 2482 × 448 mm |
| Flat patterns produced | 2 |
Result of the example
| Plate 1 | 2482 × 224 mm, cut 2 times |
|---|---|
| Plate 2 | 2482 × 448 mm, cut 4 times |
Assembly notes
Weld the sheets with the longitudinal seams 180° apart, not lined up. Lined up, the piece assembles into a different shape — and the longitudinal seam crosses the circumferential one.
How to mark it out on the plate
- Work out β and the heights y(φ) for the dv elements (16 in the example), or copy them from the calculator table.
- Mark a rectangle of L by y_heel for the end gore, divide L into dv parts and mark the height of each element from the base, heel at one edge and throat in the middle.
- Join the points with a flexible rule: the edge is a sine wave of amplitude 2 × r × tan β (111 mm in the example).
- For the middle gore mirror the same wave downwards: the rectangle is 2 × y_heel high with both edges cut.
- Cut 2 ends and (gores − 1) middles, roll each as a shell and assemble turning each gore half a turn from its neighbour: the longitudinal seams sit 180° apart.
Common mistakes and tolerances
- Radius under half the diameter
- With R < D/2 the gores cross at the throat and there is no part; the calculation refuses it. In practice R of 1 to 1.5 diameters is used.
- More than 90° per gore
- Each gore can turn at most 90° (β = 45°, the elbow cut). A 90° bend in 1 gore is the mitred elbow; with 2 it is already a bend.
- Seams in line
- With all the longitudinal seams on one side the bend assembles crooked and the longitudinal weld runs into the circumferential one. Turn each gore half a turn.
- Using the outside diameter for the circumference
- The rolled-shell mistake: π × t extra on every gore, 31.4 mm in the example in 10 mm plate.
- Confusing the axis radius with the heel radius
- R is the radius at the tube axis. The heel sits at R + D/2 and the throat at R − D/2; measuring at the throat and entering that as R gives a tighter bend.
Guides about this part
Frequently asked questions
- How many gores should I use?
- It is the trade between finish and work: more gores follow the radius better and reduce pressure loss, but mean more cuts and more welding. For a 90 degree exhaust bend, three to five usually does it.
- What is measurement H?
- The bend radius measured at the tube axis. The calculation requires it to be at least half the diameter, or the gores would intersect.
- How many plates come out of a 5-gore bend?
- Two different ones, six plates: the half end, cut twice, and the full gore, cut four times. In the example, 2482 × 224 mm and 2482 × 448 mm.
- What is the half-mitre?
- The cut angle of each gore from square: β = total angle / (2 × gores). For 80° in 5 gores, 8°. It is what goes into the cut-height formula, (R + r × cos φ) × tan β.