Offset Rectangular Transition flat pattern
What it is
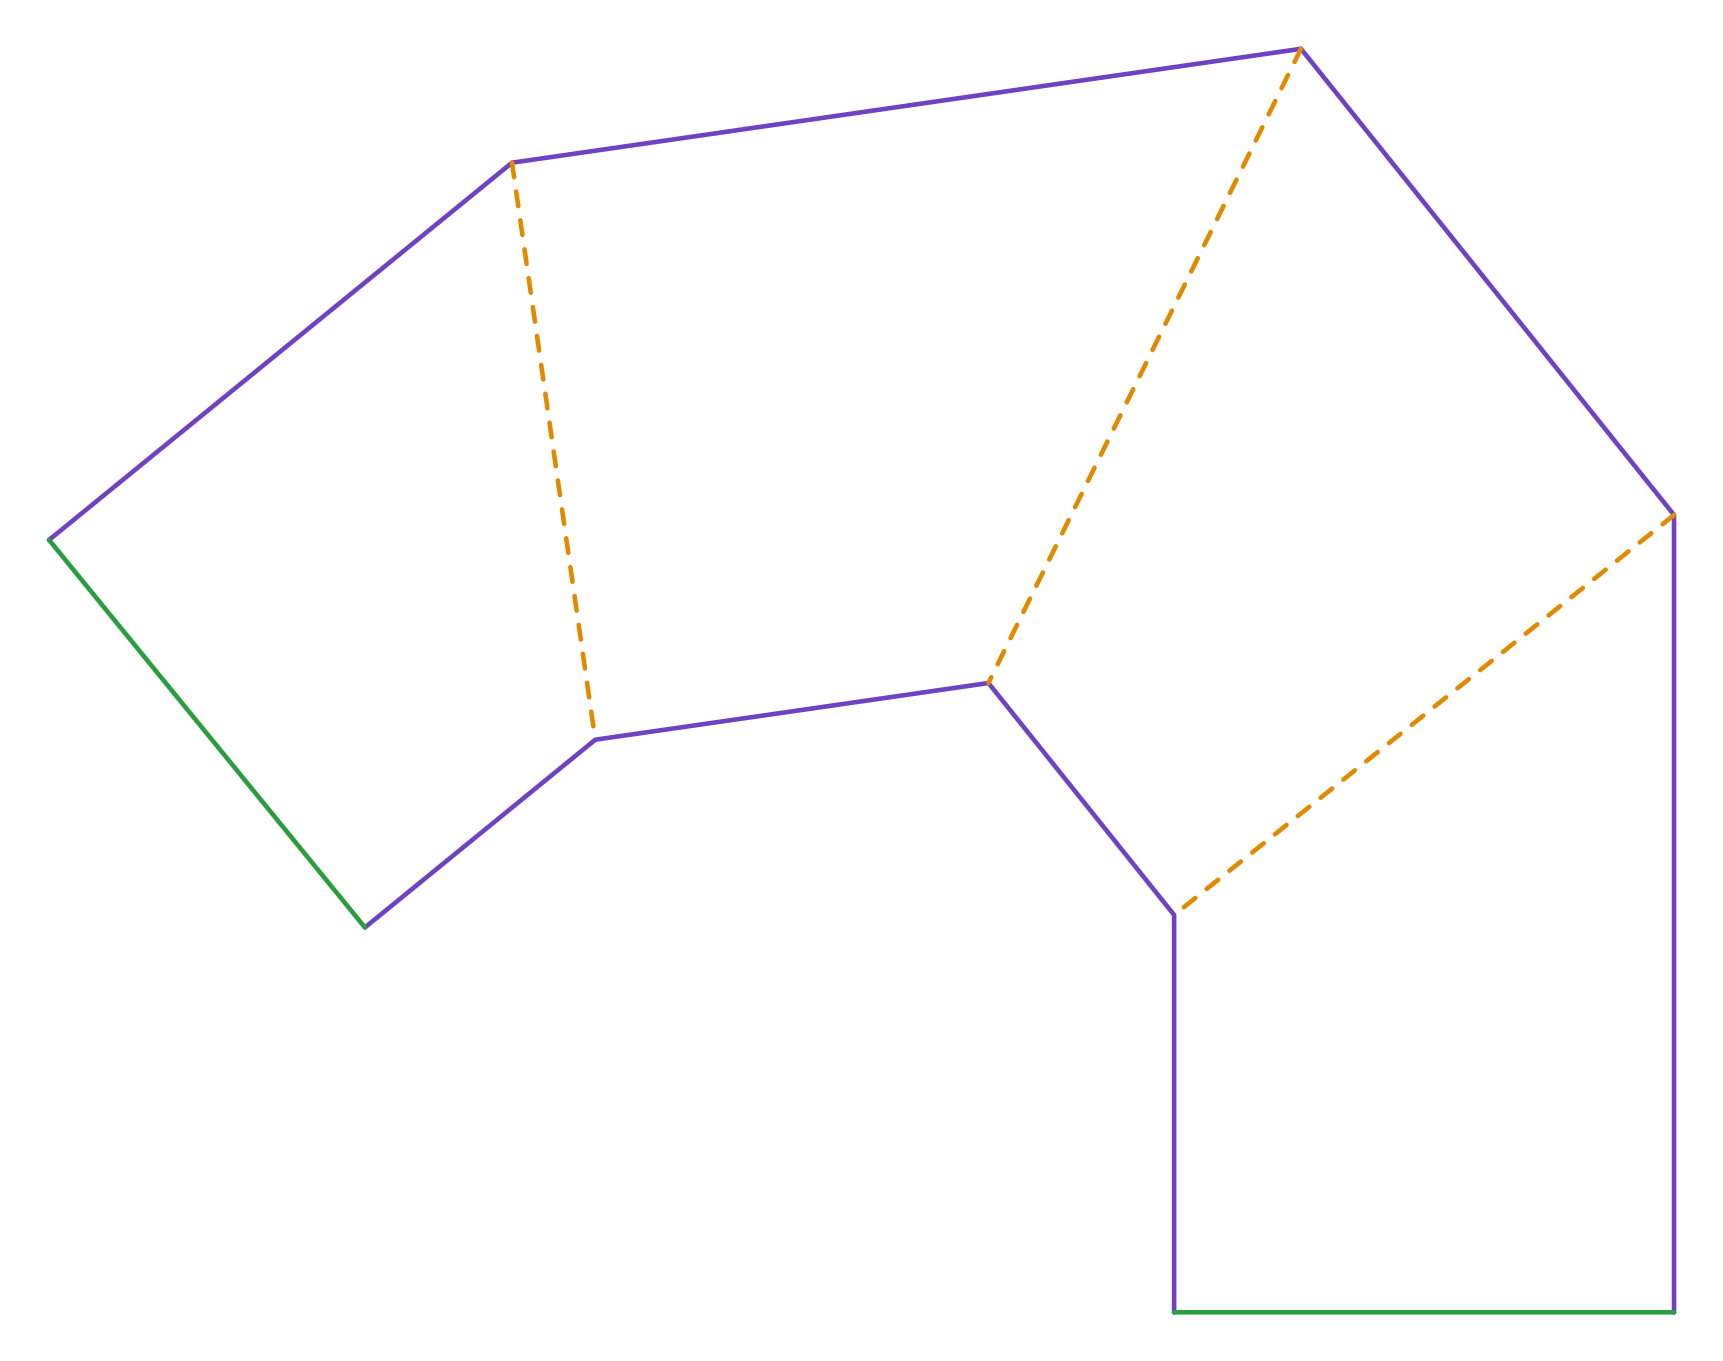
The rectangular reducer with the top opening off the axis of the bottom one: the offset transition of the duct shop, and the hopper with its outlet to one side. Moving the opening does not warp any face. Each top edge stays parallel to its bottom edge, so the four faces are still flat trapezoids and the pattern is exact, with no triangulation. What changes is that the four faces all differ, each with its own slant and its own sideways shift, and no sheet repeats another.
Where it is used
Plenum transitions from a furnace or air handler down to the supply trunk, duct transitions that run flat against a ceiling or a wall, hoppers and bins with the outlet to one side, chutes and fan connections off the axis.
Measurements the calculation needs
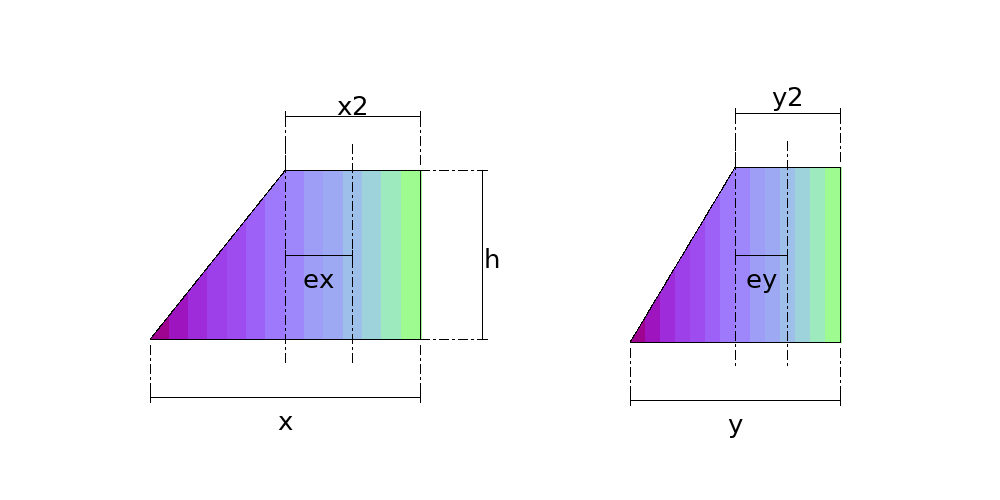
- X Side X of the bottom mouth
- Y Side Y of the bottom mouth
- X2 Side X of the top mouth
- Y2 Side Y of the top mouth
- EX Offset of the top mouth in X
- EY Offset of the top mouth in Y
- H Height between the mouths
- THK Plate thickness
- NP Number of sheets
- SB Pittsburgh pocket allowance
- SA Pittsburgh flange allowance
- SP End allowance (TDC, S and drive)
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Inches or millimetres? mm inches
How it develops: the formulas
- Slant height of each face
h1 = √( h² + ((Y − Y2)/2 − ey)² ) ; h2 = √( h² + ((X − X2)/2 + ex)² ) ; h3 = √( h² + ((Y − Y2)/2 + ey)² ) ; h4 = √( h² + ((X − X2)/2 − ex)² )One per face, going round: the X face on the +Y side, the Y face on the −X side, the X face on the −Y side and the Y face on the +X side. In the example (800 × 600 to 400 × 300, offset 200 in X and 150 in Y, h = 500): 500.0, 640.3, 583.1 and 500.0 mm.- Sideways shift of the top edge
X faces: (X − X2)/2 − ex and (X − X2)/2 + ex from the corner ; Y faces: (Y − Y2)/2 − ey and (Y − Y2)/2 + eyOn the concentric reducer the top edge sits centred over the bottom one. Here it slides along it by the offset, and where the shift comes out zero the face has a square corner, as on two faces of the example.- Angle between neighbouring faces
the dihedral between the two face planes, corner by cornerIn the example the three corners that touch a plumb face are at 90° and the corner opposite the offset at 108.7°. The assembly note gives all four.
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Side X of the bottom mouth | 800 mm |
|---|---|
| Side Y of the bottom mouth | 600 mm |
| Side X of the top mouth | 400 mm |
| Side Y of the top mouth | 300 mm |
| Offset of the top mouth in X | 200 mm |
| Offset of the top mouth in Y | 150 mm |
| Height between the mouths | 500 mm |
| Plate thickness | 3 mm |
| Number of sheets | One sheet (the whole piece) |
| Pittsburgh pocket allowance | 0 mm |
| Pittsburgh flange allowance | 0 mm |
| End allowance (TDC, S and drive) | 0 mm |
| The flat pattern fits a plate of | 1625 × 1264 mm |
Result of the example
| Plate | 1625 × 1264 mm |
|---|---|
| Area and weight | 1.16 m² · ≈ 27.2 kg in 3 mm steel |
Assembly notes
The pattern develops the SHARP CORNER, on the mean line — the theoretical layout, which is what gets delivered. If you fold it on a press brake with an inside radius, the blank comes out LONG: each fold needs, against this pattern, the deduction 2*(r+t/2)*tan(a/2) − a*(r + k*t), with r the inside radius, a the bend angle in radians, and your tooling's k. On a 500x300 tube in 1.5 mm sheet with four 90° folds that is 3.6 mm at radius 0.75 and 9.3 mm at radius 4.5 — always to be taken off. A welded or V-notched corner closes on the sharp corner and needs no deduction.
The walls are flat, because the top opening is parallel to the base, and each corner has a single angle along its whole length. But with the opening offset both ways, every corner has its own angle BETWEEN THE FACES: 90° at the corner the opening moves towards, 108.7° at the opposite corner, 90° at the other corner on the side it moves to along X, and 90° at the other corner on the side it moves to along Y. Measure with a protractor on the finished part, not by the press stroke.
How to mark it out on the plate
- Work out the four slant heights, one per face. Mark the faces in sequence, joined along the sloping corner edges, with the seam on a corner.
- On each face mark the base (X or Y), go up its slant height square to the base, and mark the top opening (X2 or Y2) shifted along the base: from the corner, (X − X2)/2 ∓ ex on the X faces and (Y − Y2)/2 ∓ ey on the Y faces.
- Check that each corner edge measures the same on the two faces that share it, then crease and fold each corner to its own angle.
Common mistakes and tolerances
- Centring the top opening on every face
- That is the concentric reducer. With the offset the top edge slides along the bottom one and each face has its own slant height: from 500.0 to 640.3 mm in the example.
- Folding every corner to the same angle
- Only the concentric reducer has four equal corners. Here each one has its own, 90° and 108.7° in the example, and folded to a single angle the top opening does not land where it should.
Guides about this part
- Duct transition layout: square to round duct, centred, offset or flat on one side
- Plenum box and plenum transition layout: the sides, the end cap, the collar and the transitions
Frequently asked questions
- Where is the offset measured from?
- From the centre of the bottom opening to the centre of the top one, split into X and Y, as on the eccentric rectangle to round. Zero in both gives back the concentric rectangular transition, face for face.
- How do I make it flat on one side?
- Make the offset half the difference on that side. With X = 800 and X2 = 400, an offset of 200 in X puts the top opening flush with the bottom one on that side, and the face there comes out plumb: the flat on top or flat on bottom of a duct drawing. The example is flat on two sides, X and Y, the duct that runs tight against a ceiling and a wall.
- Can the top opening go past the edge of the bottom one?
- Yes. Past half the difference the opening leaves the outline of the bottom one, and the face on that side leans outwards instead of in. The face is still a flat trapezoid and the calculation does not change, so it sets no limit on the offset.
- Why are the four faces all different?
- Because each one leans its own amount. The face on the side the opening moves towards stands steeper and the opposite one lies flatter, and on the other two the top edge slides along the bottom one by the offset. In the example the slant heights are 500.0, 640.3, 583.1 and 500.0 mm. On the concentric reducer they come in two equal pairs; here no sheet repeats another, so cut one of each.
- What angle does each corner fold to?
- Each corner has its own angle between the faces, and the assembly note gives all four. In the example the three corners that touch a plumb face are at 90°, and the corner opposite the offset is at 108.7°.
- Does it come out in two or four sheets, with the Pittsburgh allowances?
- Yes, as on the concentric reducer: two L-shaped sheets or the four faces apart, in the Number of sheets field, and the pocket, flange and end allowances if you enter them. The pocket goes on the faces of the short side of the duct, and each seam joins two edges of the same length.
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.