Truncated Cylinder flat pattern
What it is
A rolled shell cut on an inclined plane at one end — a mitre cut. Developed, the cut edge becomes a sine wave: its height comes from the cut angle and its length from the circumference of the shell.
Where it is used
Pipe entering an inclined wall, discharge openings, column feet cut to floor angle, roof penetrations.
Measurements the calculation needs
- D Outside diameter of the shell
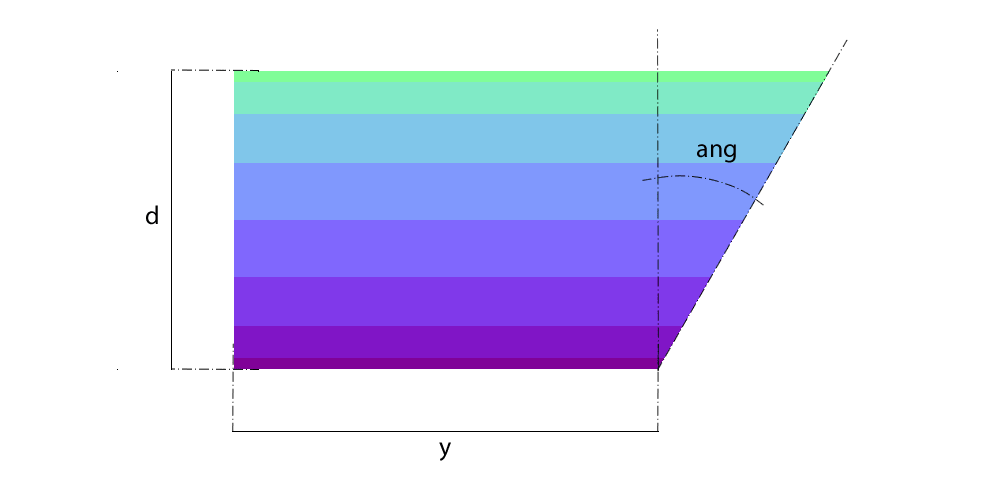
- Y Height of the shorter side
- ANG Cut angle (from a square cut)
- DV Divisions
- THK Plate thickness
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Units: mm inches
How it develops: the formulas
- Plate length
L = π × (D − t)In the example, D = 200 in 10 mm plate: L = 596.9 mm.- Height at each element
z(φ) = y + (t/2) × tan α + r × tan α × (1 − cos φ)r = (D − t)/2 is the mean radius, α the cut angle to the horizontal and φ the angle round the tube from the low side. With dv divisions, φ advances 360°/dv per element.- High side
z_max = y + (t/2) × tan α + (D − t) × tan αIn the example (y = 50, α = 40°): 54.2 + 159.4 = 213.6 mm. The plate is 597 × 214.- Wave amplitude
A = (D − t) × tan αThe difference between the high and low sides of the cut: 159.4 mm in the example.
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Outside diameter of the shell | 7-7/8" (7.874) |
|---|---|
| Height of the shorter side | 1-15/16" (1.9685) |
| Cut angle (from a square cut) | 40° |
| Divisions | 16 |
| Plate thickness | 3/8" (0.3937) |
| The flat pattern fits a plate of | 23-1/2" × 8-7/16" |
Result of the example
| Plate | 23-1/2" × 8-7/16" |
|---|---|
| Area and weight | 0.86 ft² · ≈ 13.8 lb in 3/8" steel |
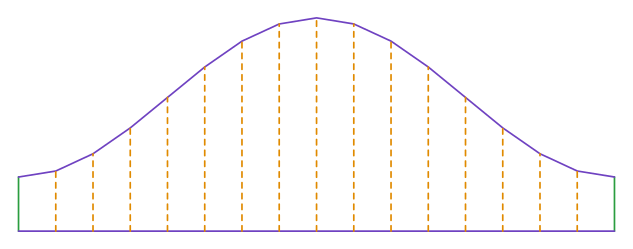
Ordinate table
| # | Position on the plate | Element height |
|---|---|---|
| 1 | 0" | 2-1/8" |
| 2 | 1-7/16" | 2-3/8" |
| 3 | 2-15/16" | 3-1/16" |
| 4 | 4-3/8" | 4-1/16" |
| 5 | 5-7/8" | 5-1/4" |
| 6 | 7-5/16" | 6-1/2" |
| 7 | 8-13/16" | 7-1/2" |
| 8 | 10-1/4" | 8-3/16" |
| 9 | 11-3/4" | 8-7/16" |
| 10 | 13-1/4" | 8-3/16" |
| 11 | 14-11/16" | 7-1/2" |
| 12 | 16-3/16" | 6-1/2" |
| 13 | 17-5/8" | 5-1/4" |
| 14 | 19-1/8" | 4-1/16" |
| 15 | 20-9/16" | 3-1/16" |
| 16 | 22-1/16" | 2-3/8" |
| 17 | 23-1/2" | 2-1/8" |
How to mark it out on the plate
- Mark the rectangle of L by z_max and divide L into dv equal parts (16 in the example): each division is an element line.
- Work out z for each element from the formula, or copy it from the calculator table, and mark the height on each from the base.
- Join the points with a flexible rule: the curve is a sine wave, low at the seam and high on the opposite side.
- Cut the curve, roll and weld the seam on the low side, which is the shortest element and the shortest weld.
Common mistakes and tolerances
- Entering the high side as y
- y is the LOW side, where the cut meets the shell. The high side follows from the formula.
- Joining the points with a straight edge
- Between two elements the edge is curved. With 16 divisions the chord error is small; with 8 it already shows as facets on the mouth.
- A 90° angle
- At α = 90° the cutting plane is parallel to the axis and cuts no mouth; the calculation refuses it. Close to 90° gives a part that is enormous on one side.
Guides about this part
- How to lay out a mitre-cut pipe: paper template, sine wave and ordinate table
- Tube notching template generator: a printable coping template for any tube, angle and offset
- Pipe template, printable at full size: tee saddle, 45° lateral and mitre cut for every pipe size from NPS 1/2 to 12
Frequently asked questions
- What is measurement Y?
- The height of the short side of the part, taken where the inclined cut meets the shell. The tall side follows from the angle you enter.
- Why does the cut edge become a wave rather than a straight line?
- Because when the cylinder is unrolled, every point on the inclined opening was at a different height. That variation, spread along the circumference, traces exactly a sine wave.
- How high is the high side in the example?
- For 200 diameter, a 50 low side, a 40° cut and 10 mm plate: 213.6 mm. It is y + (t/2) × tan α + (D − t) × tan α, and the plate comes out 597 × 214.
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.