Rectangular Tap on a Cone development
What it is
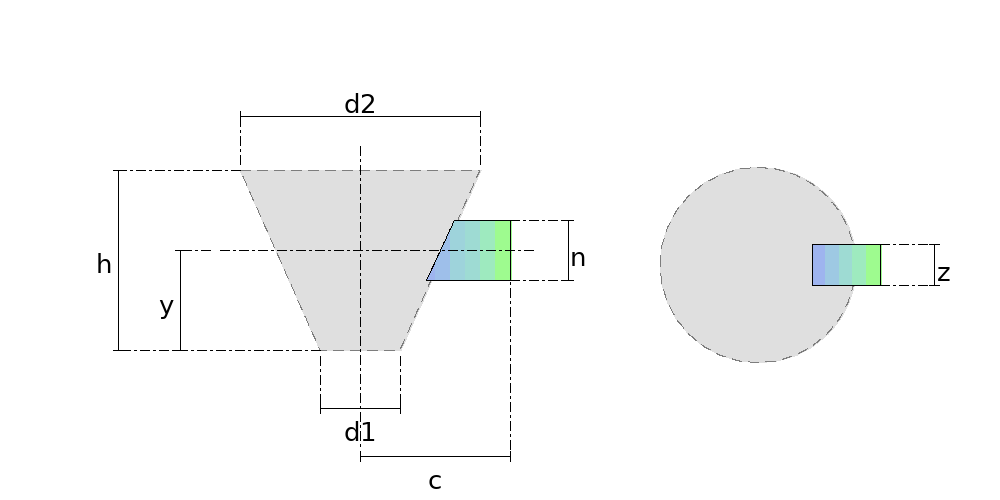
The rectangular collar seated on the wall of a truncated cone, its axis horizontal and crossing the cone's axis. It is the grille mouth and the chute on a conical hopper — the same part as the rectangular tap on pipe, but on a host whose radius changes with height.
Where it is used
Conical hoppers, silos, cyclone bodies, conical hoods, grille and chute mouths on any conical wall.
Measurements the calculation needs
- D1 Smaller diameter (bottom)
- D2 Larger diameter (top)
- H Height of the cone
- N Length of the mouth (along the cone axis)
- Z Width of the mouth (across the axis)
- Y Height of the mouth axis (from d1)
- C From the cone axis to the end of the mouth
- DV Divisions
- THK Plate thickness
- R Bend radius
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Smaller diameter (bottom) | 400 mm |
|---|---|
| Larger diameter (top) | 1200 mm |
| Height of the cone | 900 mm |
| Length of the mouth (along the cone axis) | 300 mm |
| Width of the mouth (across the axis) | 250 mm |
| Height of the mouth axis (from d1) | 500 mm |
| From the cone axis to the end of the mouth | 750 mm |
| Divisions | 16 |
| Plate thickness | 4 mm |
| Bend radius | 0 mm |
| The flat pattern fits a plate of | 1084 × 415 mm |
Result of the example
| Plate | 1084 × 415 mm |
|---|
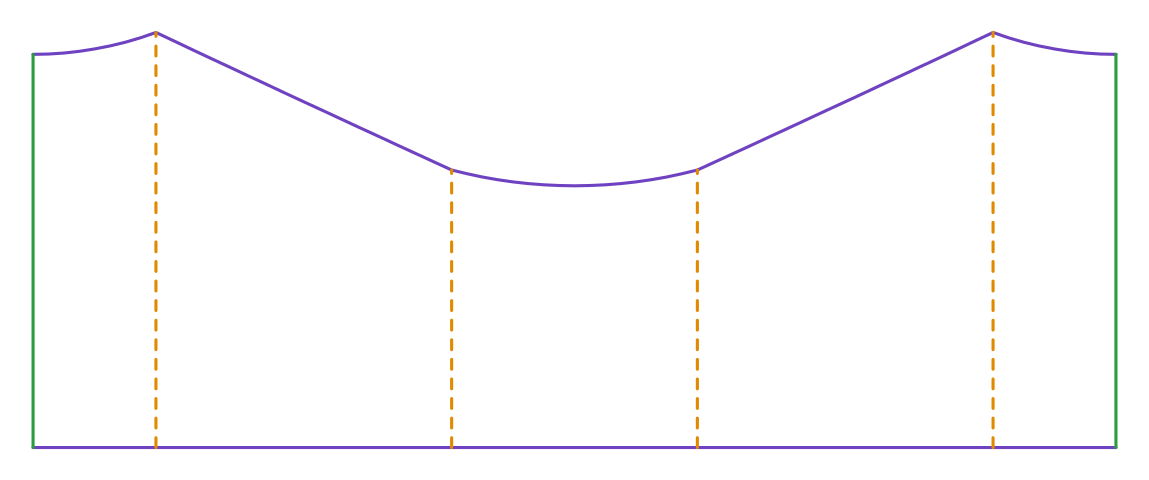
Assembly notes
The pattern develops the SHARP CORNER, on the mean line — the theoretical layout, which is what gets delivered. If you fold it on a press brake with an inside radius, the blank comes out LONG: each fold needs the deduction 2*(r+t)*tan(a/2) − a*(r + k*t), with r the inside radius, a the bend angle in radians, and your tooling's k. On a 500x300 tube in 1.5 mm sheet with four 90° folds that is 3.5 mm at radius 0.75 and 9.0 mm at radius 4.5 — always to be taken off. A welded corner from separate plates needs no deduction at all.
Fold to an angle of 90° BETWEEN THE TWO FACES — what a protractor reads on the finished part, not the press stroke angle. Every crease on this part has the same angle.
Frequently asked questions
- Which figure runs along the cone's axis?
- `n`, the mouth length. `z` runs across. It is the same rule as the rectangular tap on pipe, where the length follows the pipe's length — and it matters more here, because the two bites belong to different families: swapping the two figures does not give the same part rotated, it gives a different part.
- Why are the four bites all different?
- Because the cone changes radius with height. The two walls perpendicular to the cone's axis lie in planes of constant height, and such a plane cuts the cone in the very circle of that height: the bite is an exact arc, and the two arcs have different radii. The two parallel walls lie in planes of constant offset, and there the bite is a hyperbola. The part comes out deeper at the top than at the bottom.
- Where do I measure c from?
- From the cone's AXIS to the tip of the collar, the same datum as the cone branch. The guard asks it to clear the deepest bite, which is at the middle of the upper wall.
- What about the hole in the cone?
- That is the companion part, "Cone with Rectangular Hole" — and it is worth far more than the name suggests, because the hole is NOT a rectangle. Enter the same figures in both and the two patterns match.
An account is required. The free tier covers 20 calculations a month.