Rectangular Duct S-Offset flat pattern
What it is
The S-offset moves a duct sideways without changing its direction: the centreline runs two arcs of the same radius, one each way, and the duct leaves parallel to the way it came in, shifted across. Fitting catalogues call it an ogee offset, and it comes out the way a duct shop makes it — two flat cheeks cut to the S outline and two wrappers rolled between them. The calculation finds the radius and the turn of each arc from the offset and the length, and returns the cheeks drawn in arcs, the wrappers with the reversal marked, the 1:1 template and the DXF.
Where it is used
Air-conditioning, extraction and ventilation ductwork that has to clear a beam, a pipe or a cable tray; connecting equipment whose outlet is off the line of the run; dust collection and pneumatic conveying in rectangular section.
Measurements the calculation needs
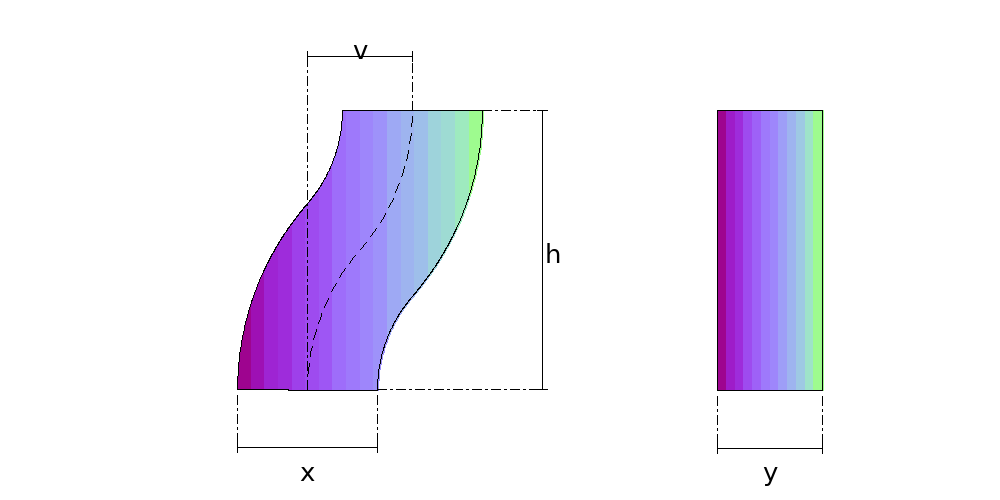
- X Duct side in the plane of the offset
- Y Duct side across the offset
- V Offset between the centrelines
- H Length of the offset, along the duct
- THK Plate thickness
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Inches or millimetres? mm inches
How it develops: the formulas
- Radius and turn of each arc
R = (v² + h²) / (4 × v) ; θ = 2 × arctan(v / h)v is the offset between the centrelines and h the length of the offset, along the duct. It is the reverse curve of surveying: v = 2R × (1 − cos θ) and h = 2R × sin θ. In the example, 300 over 800: R = 608.3 mm and θ = 41.1°.- The cheek edges
Rt = R − x/2 ; Rh = R + x/2Round the first centre the inner side has radius Rt and the outer Rh; round the second, 2R from the first, the sides swap. In the example, a 400 duct: 408.3 and 808.3 mm.- The length of the wrappers
L = 2 × R × θ ; reversal at (R + (x − t)/2) × θ from one endBoth wrappers measure the length of the centreline, 873.0 mm in the example, and fit between the cheeks at width y − 2t. The curve reverses 579.5 mm from one end.
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Duct side in the plane of the offset | 400 mm |
|---|---|
| Duct side across the offset | 300 mm |
| Offset between the centrelines | 300 mm |
| Length of the offset, along the duct | 800 mm |
| Plate thickness | 1.5 mm |
| The flat pattern fits a plate of | 873 × 700 mm |
| Flat patterns produced | 2 |
Result of the example
| Plate 1 | 800 × 700 mm, cut 2 times |
|---|---|
| Area and weight | 0.35 m² · ≈ 4.1 kg in 1.5 mm steel |
| Arc radii | 408.3 mm · 808.3 mm |
| Sector angle | 41.1° |
| Plate 2 | 873 × 297 mm, cut 2 times |
| Area and weight | 0.26 m² · ≈ 3.1 kg in 1.5 mm steel |
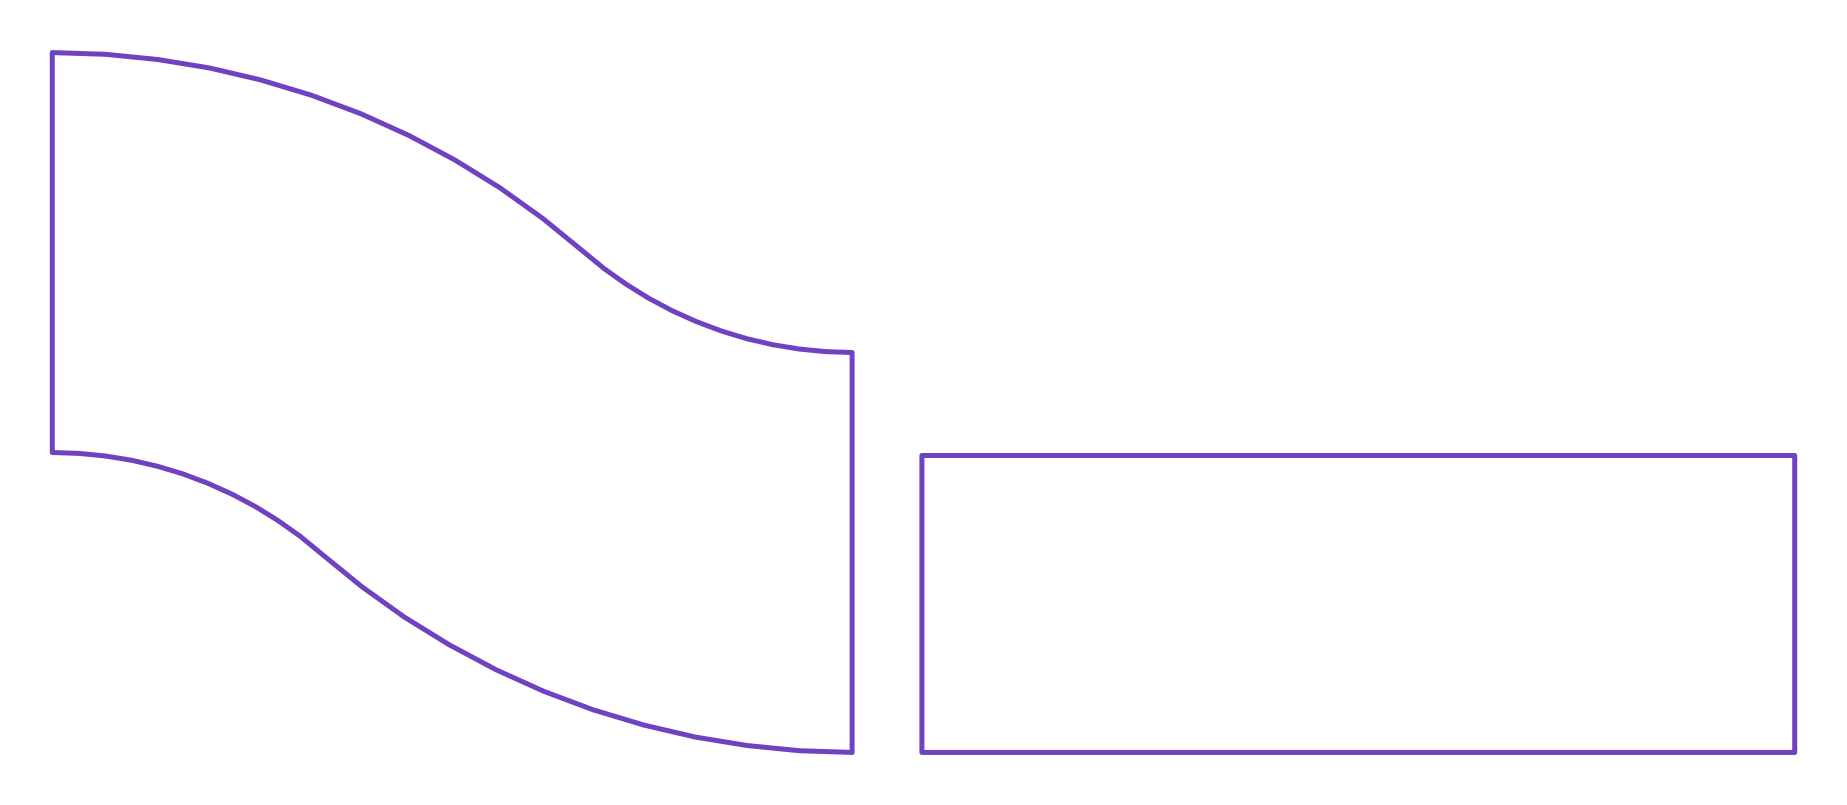
Assembly notes
Sheet 1 is the two CHEEKS, flat and identical, cut to the outside outline of the duct. Sheet 2 is the two WRAPPERS, also identical, at the inside width, 297 mm: they fit between the cheeks and are welded to their curved edges.
Each wrapper is rolled into an S, and the dimension on sheet 2 marks the reversal: over the 579.5 mm stretch it seats on the cheek's 808.3 mm radius edge, and over the 293.5 mm stretch it curves the other way and seats on the 408.3 mm radius edge. Fit the two wrappers half a turn round from each other: the large-radius stretch of one faces the small-radius stretch of the other.
How to mark it out on the plate
- Enter the duct (x in the plane of the offset, y across it), the offset between the centrelines, the length of the offset and the thickness.
- Cut two cheeks from the template. To mark one out by hand: the first centre lies on the line of the inlet, Rt from its inner corner; strike the arcs of radius Rt and Rh through θ, and the second centre lies on the line of the reversal, 2R from the first.
- Cut two wrappers of L by y − 2t and mark the reversal on both long edges.
- Roll each wrapper into an S: the longer stretch to the outer radius, the other the opposite way to the inner radius.
- Fit the wrappers between the cheeks, one half a turn round from the other, and weld the four edges.
Common mistakes and tolerances
- Wrappers of different lengths
- Working out one wrapper on the inner radius and the other on the outer radius gets both wrong: each wrapper is inner on one arc and outer on the other, and both measure the centreline, 2 × R × θ.
- Rolling the whole wrapper the same way
- An offset wrapper is an S: the curve reverses at the mark. Mark it before rolling.
- Fitting both wrappers the same way round
- One is the other turned half a turn: the large-radius stretch of one faces the small-radius stretch of the other.
Frequently asked questions
- How do you work out the radius of an S-offset?
- From the offset v and the length h: R = (v² + h²) / (4 × v) on the duct centreline, and each arc turns θ = 2 × arctan(v / h). In the example, 300 of offset over 800 of length: R = 608.3 mm and θ = 41.1°. The cheek edges have radii R − x/2 and R + x/2: 408.3 and 808.3 mm for a 400 duct.
- Why do the two wrappers come out the same?
- Because each wrapper is the heel on one arc and the throat on the other, and what it gains on the first it loses on the second: both measure 2 × R × θ, the length of the centreline — 873.0 mm in the example. What differs is which end the curve reverses from, and the reversal is marked on the sheet: 579.5 mm from one end and 293.5 from the other.
- Do the wrappers go inside or outside the cheeks?
- Inside. The cheeks are cut to the outside outline of the duct and the wrappers fit between them, at the inside width, y − 2 × thickness. That is the welded build of heavy plate; on light gauge the difference is small, and the cheek template is the same.
- What is the largest offset you can make?
- Equal to the length: each arc then turns 90° and the offset is two radius elbows back to back. Beyond that the S goes past square, and the run wants two 90° bends and a straight. The centreline radius must also be more than half the duct width, or the throat disappears.
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.