Oval Segmented Bend flat pattern
What it is
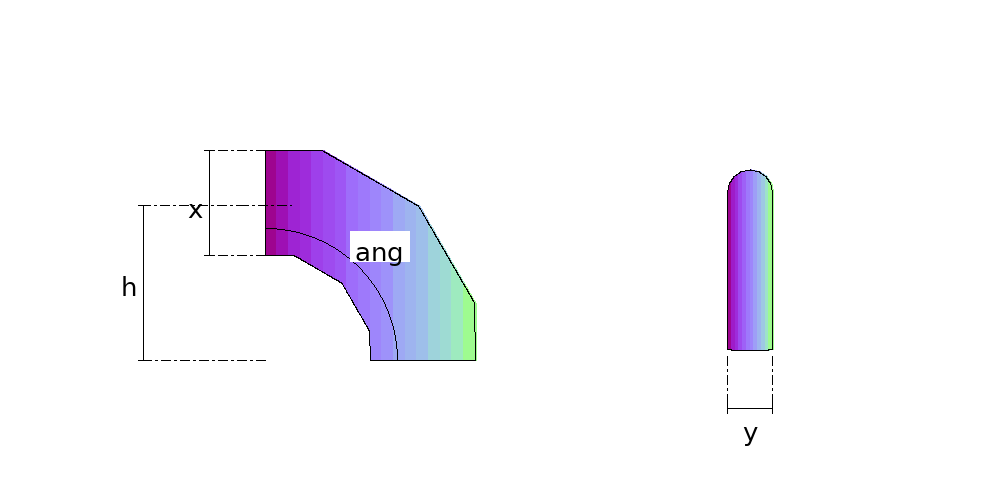
The segmented bend for OVAL duct -- the obround, two half-rounds joined by two straight runs. The catalogue already had the round segmented bend and the rectangular duct bend; this is the third sister, and it is the section of flat-oval duct, used where the headroom will not take the equivalent round.
Where it is used
Flat-oval extraction and air-conditioning duct, runs between beam and ceiling, industrial hoods, pneumatic conveying in tight spaces.
Measurements the calculation needs
- H Bend radius, from its centre to the duct axis
- X Duct measure in the plane of the bend
- Y Duct measure across it
- ANG Total angle of the bend
- S Number of gores
- DV Divisions
- THK Plate thickness
Calculate with your own measurements
No account needed: enter the measurements in millimetres or inches and get the figures and the drawing. The scaled PDF template, the DXF for the cutting table and the 3D model take a free account.
Diameters and sides are outside measurements. The flat pattern already allows for the plate thickness, working on the mean line.
Units: mm inches
Worked example
The values the form comes pre-filled with, run through the tool itself:
| Bend radius, from its centre to the duct axis | 35-7/16" (35.4331) |
|---|---|
| Duct measure in the plane of the bend | 23-5/8" (23.622) |
| Duct measure across it | 11-13/16" (11.811) |
| Total angle of the bend | 90° |
| Number of gores | 3 |
| Divisions | 16 |
| Plate thickness | 1/8" (0.1181) |
| The flat pattern fits a plate of | 60-3/8" × 25-5/16" |
| Flat patterns produced | 2 |
Result of the example
| Plate 1 | 60-3/8" × 12-5/8", cut 2 times |
|---|---|
| Area and weight | 4.0 ft² · ≈ 19.2 lb in 1/8" steel |
| Plate 2 | 60-3/8" × 25-5/16", cut 2 times |
| Area and weight | 8.0 ft² · ≈ 38.4 lb in 1/8" steel |
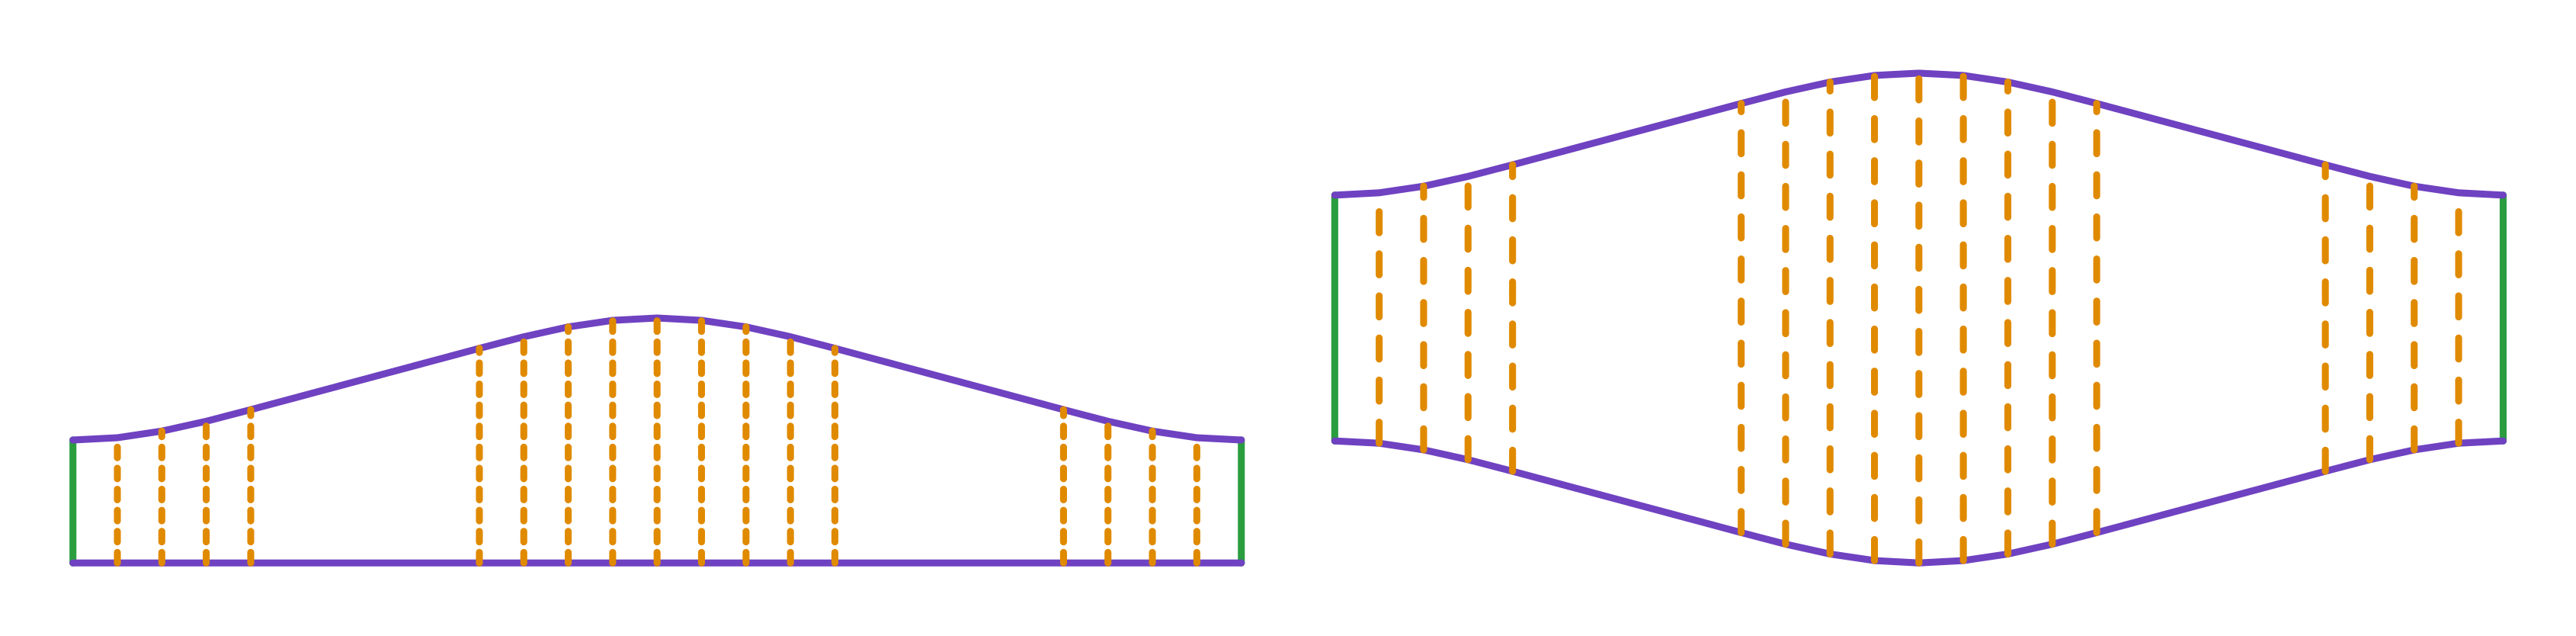
Ordinate table
| # | Position on the plate | Element height |
|---|---|---|
| 1 | 0" | 6-3/8" |
| 2 | 2-5/16" | 6-7/16" |
| 3 | 4-9/16" | 6-13/16" |
| 4 | 6-7/8" | 7-5/16" |
| 5 | 9-3/16" | 7-15/16" |
| 6 | 21" | 11-1/16" |
| 7 | 23-5/16" | 11-11/16" |
| 8 | 25-9/16" | 12-3/16" |
| 9 | 27-7/8" | 12-1/2" |
| 10 | 30-3/16" | 12-5/8" |
| 11 | 32-1/2" | 12-1/2" |
| 12 | 34-3/4" | 12-3/16" |
| 13 | 37-1/16" | 11-11/16" |
| 14 | 39-3/8" | 11-1/16" |
| 15 | 51-3/16" | 7-15/16" |
| 16 | 53-7/16" | 7-5/16" |
| 17 | 55-3/4" | 6-13/16" |
| 18 | 58-1/16" | 6-7/16" |
| 19 | 60-3/8" | 6-3/8" |
Assembly notes
Every gore comes with its longitudinal seam on the throat, the shortest weld, and the gores go together all the same way round, heel to heel. Do not turn a cut gore half a turn to stagger the seams: its long side goes to the throat and the bend loses angle. To stagger them, mark every second gore from the heel instead — cut the paper template on its middle line and swap the two halves.
Frequently asked questions
- Does it cover the oval both ways round?
- It does, on the same page. Measurement X is the one in the plane the bend turns in and Measurement Y is across it, with no requirement about which is larger -- make X larger for one orientation, Y larger for the other. It is not the same drawing rotated, which is why the shops that sell single templates charge for the two separately.
- Why is the cut not the sine curve of the round bend?
- Because the height of the cut depends on how far the point stands from the axis of the bend, and on an oval that distance follows two different paths in one lap. Round the half-rounds it varies as a cosine, as on the round bend; along the straight runs it varies linearly or stays put, as on the rectangular one. The oval cut is neither known curve -- it is the two spliced together, and that is why nobody gets this one right from memory.
- How many plates come out?
- Two different ones. The half end gore is cut twice, once at each end of the bend, and the full middle gore is cut the number of gores minus one. With a single gore the part is just the two half ends and there is no middle gore.
- Does the throat come out square?
- It depends on the orientation, and it is worth checking before marking out. With Measurement Y larger, the throat and the heel are the STRAIGHT runs, all at the same distance from the axis, so the cut does not vary along them -- it comes out square, however tight the bend. With Measurement X larger the throat is the half-round, and there the cut varies point by point.
- How many gores should it have?
- By the same rule as the round bend. Each gore turns the total angle divided by their number, and none may turn more than 90 degrees -- that is the 45-degree mitre, the steepest cut still workable. More gores make a smoother bend and less pressure drop, at the cost of more welding.
You can work out the figures right here, with no account. PDF, DXF, 3D and history take an account — free, with unlimited calculations.