Dished head development
The spherical head in gores and the nozzle set into it. A sphere is not developable: the gore template is the shop layout, exact in area, and the part is formed.
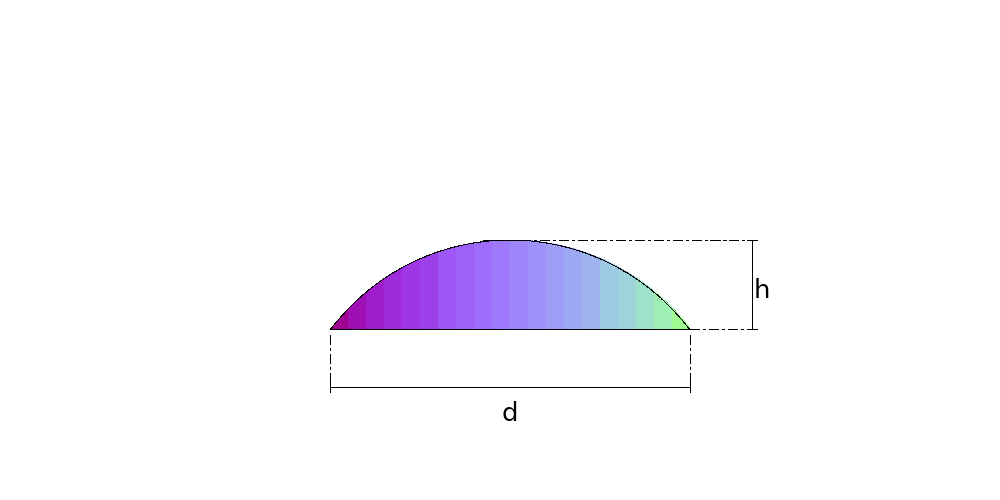
Sphere Gore (Dished Head Petal)
One gore of a spherical head. A sphere is not developable, so this is the shop layout: true length on the meridian, half-width from the parallel.
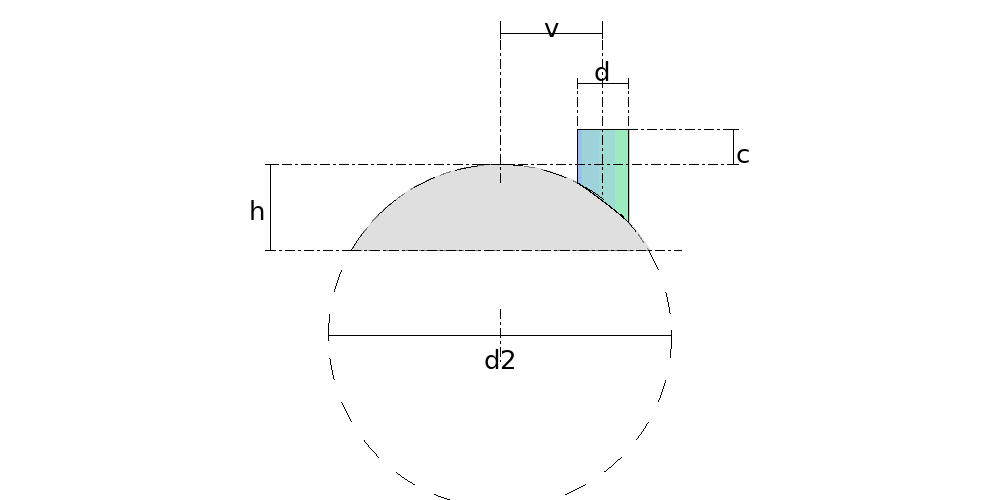
Nozzle on a Spherical Head
The upright nozzle on a formed head, its axis offset by v. The pattern is exact — the nozzle is a cylinder, and cylinders develop. The head does not.
Which part to use
- A tank or silo head made of welded gores, the spherical cap: Sphere Gore (Dished Head Petal).
- A nozzle set into a spherical head: Nozzle on a Spherical Head.
- A conical head: see Chinese Hat, in the cone family.
What the two share
A sphere is not developable: no flat plate becomes a sphere without stretching. The gore is the shop layout that comes closest, exact in area and in the length of the meridians, and the part is formed on the rolls or the press after cutting. The more gores, the less forming in each.
The dimensions are the sphere diameter, the cap height, the number of gores and the thickness; for the nozzle, its diameter and its position on the head. The result comes with the PDF template at 1:1, the DXF and the 3D view.
Frequently asked questions
- How many gores does a spherical head have?
- As many as the plate and the forming allow: fewer gores mean less welding and more forming in each; more gores, the opposite. Six to twelve is common on tank heads. The page calculates the template for the number you choose.
- Is the gore template exact?
- Exact in area and along the meridians, which is why the plate closes once formed; not exact at every point, because a sphere has no true development. It is the layout boiler shops have always used for gored heads.
- Is the nozzle on the head the same as a saddle branch?
- The idea is the same, the branch cut by the surface that receives it, but the surface here is a sphere and the intersection curve is different. The Nozzle on a Spherical Head page delivers the branch with the right wave.